
Laminating RO4350B cores into an otherwise FR-4 stack-up is the standard way to keep an RF design affordable. This guide covers the cost arithmetic, the mixed-dielectric impedance question and a checklist for qualifying a hybrid-capable manufacturer — the process-level detail lives in the companion lamination and ENIG guides.
What a Hybrid Stack-Up Actually Is
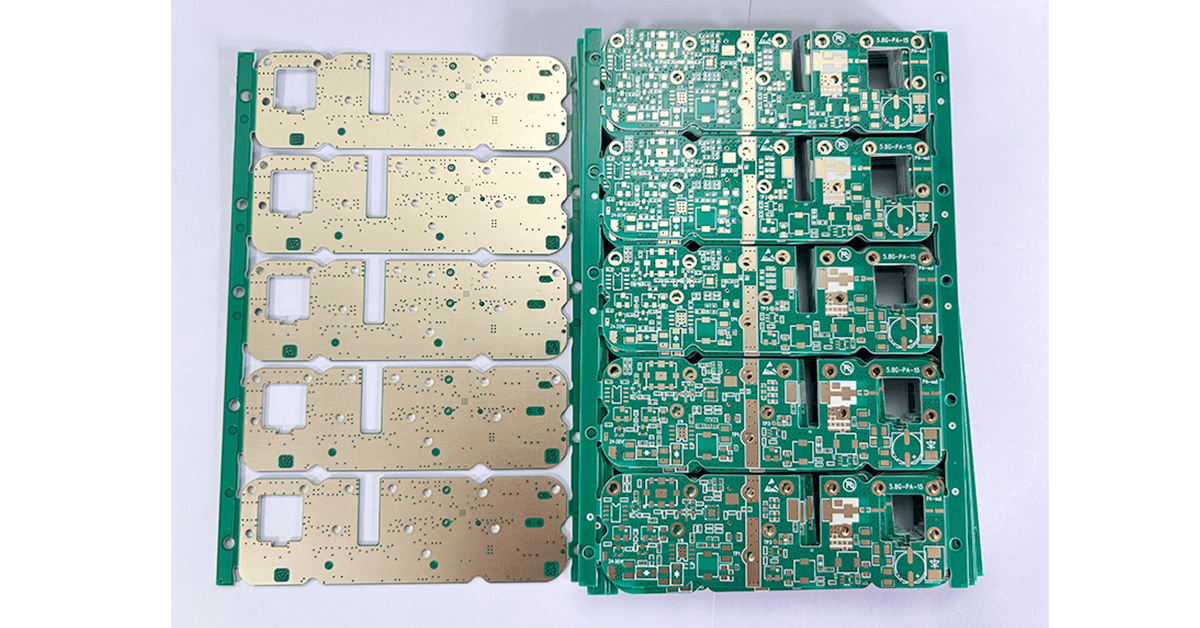
A hybrid laminate PCB carries two or more different dielectric materials in one laminated board. In the combination this page is about, RO4350B cores carry the RF and high-speed signal layers, while standard FR-4 cores and prepreg build the power, ground and low-speed digital layers. The RF signals never leave the low-loss material; the rest of the board costs what ordinary multilayer work costs.
The combination works because RO4350B is not a PTFE material. It is a glass-reinforced hydrocarbon/ceramic thermoset, which means it laminates, drills and plates on a standard FR-4 line — no sodium-naphthalene or plasma activation of through-holes, none of the special handling that a full PTFE build demands. That single property is what makes the hybrid approach practical rather than exotic: the incremental process cost over an ordinary FR-4 board is close to zero, and the material premium applies only to the layers that need it.
The reasoning parallels what we cover in the general guide to mixing Rogers materials with FR-4 — but that article is about the difficulties in the abstract. This one is about the decision: when the hybrid pays off, what it saves, and how to pick a shop that can build it.
The Cost Case: Where the Saving Actually Comes From
The economics of a hybrid rest on one observation: in most RF-containing products, the RF circuitry occupies a small fraction of the total board area. A 5G small-cell board, an automotive radar module or an instrumentation mainboard typically concentrates its antennas, filters and transceiver front end into one or two layers of the stack-up, over part of the panel. Everything else — power distribution, MCU, memory, interfaces — is ordinary digital work that FR-4 handles perfectly well at the frequencies involved.
Material spend scales with the area of high-frequency laminate used. Build the same 10-layer board two ways:
| Construction | Laminate spend | Process | RF performance |
|---|---|---|---|
| All RO4350B | Premium on 100% of the cores | Standard FR-4 line | Reference |
| Hybrid: 2 RF layers on RO4350B, rest FR-4 | Premium on the 2 cores only | Standard FR-4 line | Effectively identical for the RF nets |
| All FR-4 | Baseline | Standard FR-4 line | Not viable above ~1–2 GHz |
RO4350B laminates run from a few times to roughly ten times the per-square-metre cost of FR-4 depending on thickness and volume, so the arithmetic is intuitive: if the RF layers are two of ten cores, roughly 80% of the material premium of an all-RO4350B build disappears, with no change to the RF nets. On high-layer-count boards with large panel area the absolute saving is substantial.
The second saving is less visible but just as real: process cost does not go up at all. A full PTFE design would pay twice — once for the material, again for the special hole activation, dedicated drilling parameters and rework difficulty. The RO4350B hybrid pays neither premium on the FR-4 portion, and no process premium at all, because RO4350B itself rides the standard line. That is the entire reason the RO4000 family was created.
The honest caveat: the hybrid is a cost optimisation for boards whose RF content is localised. If nearly every layer carries controlled-impedance RF structure — a multi-layer antenna feed network, for instance — the saving shrinks toward zero and a full RO4350B build is simpler to qualify.
Electrical Performance: What the RF Layers Actually Get
On their own cores, the RF layers behave exactly as they would on a full RO4350B board: Dk 3.48 ± 0.05 at 10 GHz with a dissipation factor of 0.0037, temperature coefficient of Dk +50 ppm/°C over −50 to +150 °C, and a Z-axis CTE of 32 ppm/°C. These are the RO4000-family values that made the material the default for base station power amplifiers, and they apply unchanged in a hybrid build because the RF nets live entirely on the RO4350B cores.
Two details deserve attention at the design stage. First, plan the ground referencing so that every controlled-impedance trace sees RO4350B directly above and below it, or at minimum has its reference plane on an adjacent RO4350B layer — a stripline sandwiched between an RO4350B core and an FR-4 prepreg has a different effective Dk than the solver default assumes. Second, treat the material interface as a real boundary: signals that must cross from the RF section into the digital section should do so on a via placed away from the interface, not on a trace running across the dielectric transition, which produces a local impedance step.
For RF performance below roughly 6 GHz and through the millimetre-wave bands, a properly referenced hybrid loses nothing measurable against the all-premium build. The difference between the two exists on the drawing and the invoice, not in the network analyser.
Impedance Control With Mixed Dielectrics
Impedance in a hybrid needs more care than in a homogeneous build, because a trace may sit over or under materials with different dielectric constants within the same stack-up. Three working rules cover most of it:
1. Use the design Dk, not the process Dk. Rogers specifies process Dk 3.48 (the tight-tolerance value) and design Dk 3.66 for circuit design. Field-solver models built on 3.48 come out with impedances roughly 1.5 Ω high for 50 Ω targets. And if the stack uses the thin 0.101 mm RO4350B core, its Dk is specified as 3.36 — a datasheet footnote that silently breaks calculations done at 3.48.
2. Model the actual mixed-dielectric cross-section. Modern field solvers handle multiple dielectric regions per layer natively; older closed-form calculators do not. Where a trace sees FR-4 on one side and RO4350B on the other, the effective Dk sits between the two and the only trustworthy number comes from the solver — ideally one calibrated against the manufacturer’s measured coupons.
3. Verify on the production panel, not just in the model. We hold impedance to ±10% by specification and verify it with TDR coupons processed on the same panel as the order. On hybrids the coupon should reproduce the real layer sequence, because a single-material coupon cannot see a mixed-dielectric error.
Reliability Rules: Managing the CTE Mismatch
Dissimilar materials joined at high temperature and cycled in service will try to move relative to each other, and the stack-up has to be designed for it. The numbers: RO4350B expands 10/12/32 ppm/°C in X/Y/Z, close to copper in-plane; FR-4 runs roughly 50–70 ppm/°C in Z (higher above Tg). The mismatch concentrates in the Z direction — exactly the direction the copper barrels of the vias run — and peaks at lamination and reflow temperatures.
Three measures keep it managed, all of them standard practice in hybrid work:
Symmetrical stack-up. Mirror material types, copper weights and pattern density about the board’s centre plane — the classic RO4350B core centred in FR-4, or RO4350B cores mirrored in pairs. Asymmetric builds accumulate warp that shows up at reflow.
Compatible prepreg at the interface. The bonding layers touching the RO4350B cores should be chosen for adhesion to both chemistries; the lamination profile then ramps temperature and pressure so both resin systems flow and cure without trapping stress. This is manufacturing detail, and it is covered properly in the hybrid lamination process analysis.
Via placement and filling. Keep the highest-reliability vias out of the immediate neighbourhood of the material boundary, and use filled-and-capped construction for vias that must survive many thermal cycles. In-plane, both materials track copper closely, so the lateral stress problem is minor — the design effort belongs in Z.
Choosing a Manufacturer: The Qualification Checklist
Hybrid boards fail at the seam between design intent and shop-floor practice, and that seam is exactly where an inexperienced fabricator hides. The questions below separate the two in one phone call:
| Ask | What a capable shop answers |
|---|---|
| Have you built RO4350B + FR-4 hybrids in production, not just samples? | Yes, with references or case details, and a preferred stack-up template |
| Will you review our stack-up before quoting? | Yes — symmetry, reference planes, via placement and prepreg choice all get comments before the PO |
| What impedance tolerance can you hold, and how is it verified? | ±10% or better, verified by TDR coupon in the real layer sequence, on the production panel |
| What lamination profile do you use for hybrids? | A defined ramp/pressure profile for mixed resin systems, not “same as FR-4” |
| What comes back with the first article? | Micro-sections across the material interface and thermal-stress or solder-float test data on request |
The stack-up review is the most predictive single question. A shop that quotes without commenting on symmetry or reference planes is pricing your drawing, not engineering it — and the first reflow cycle will find the difference.
Where the Hybrid Is the Wrong Answer
The combination is powerful but not universal, and the failed projects we see follow three patterns:
Everything is RF. When most layers carry controlled-impedance structure, the saving evaporates and the hybrid adds interface risk for no return. Build it all on RO4350B — it is still far cheaper than PTFE alternatives.
The loss budget is already tight at millimetre wave. Df 0.0037 is excellent next to FR-4 and ordinary next to the PTFE laminates; at 77 GHz a long feed network on RO4350B spends real dB. If the budget is marginal, compare against RO4003C at Df 0.0027 before abandoning the RO4000 family — the hybrid logic stays the same either way.
FR-4 layers carry fast digital edges. The hybrid optimises for RF, not for signal-integrity-critical digital. Multi-gigabit serial links can live on the RO4350B portion too — put them there, or accept the loss and reflection budget on FR-4 knowingly.
And one selection note: the choice of surface finish interacts with the RF layer, which is why immersion gold (ENIG) has become the default finish for hybrid RF boards — flat pads for fine-pitch devices, no tape-and-reflow thickness variation under antennas, and low surface roughness for the highest bands.
Typical Applications
| Application | On RO4350B | On FR-4 |
|---|---|---|
| 5G base station / small cell | Antenna feed, PA, LNA, transceiver front end | Power distribution, baseband, control |
| Automotive radar (77 / 79 GHz) | RF traces to the radar transceiver | MCU, CAN/LIN interfaces, power |
| Microwave point-to-point links | RF front end | Digital processing unit |
| Test and measurement | Critical input/output channels | Internal digital and display sections |
Across all four, the pattern is the same: a compact RF region inside a much larger conventional board. That is the shape of problem the hybrid was invented for — and where the cost case from the section above delivers in full.
How XCE PCB Builds RO4350B + FR-4 Hybrids
Hybrid stack-ups are routine for us, not a special request: RO4350B cores laminated into FR-4 builds, 2 to 72 layers, impedance controlled to ±10% and verified with TDR coupons in the true layer sequence, panels up to 600 × 1200 mm. Samples in as fast as 24 hours when laminate is in stock.
Every hybrid order starts with a stack-up review — symmetry, reference planes, prepreg selection at the RO4350B interface and via strategy — before we quote, because a problem found there costs nothing and the same problem found at first article costs a rebuild. For a view of how the cost/performance trade is usually decided, see RO4350B as the balance point between RF performance and manufacturing cost.
Send us the stack-up, the frequency band and the volume forecast. We will come back with a quote, the impedance model assumptions, and — where we think a different construction serves the product better — a straight answer about that too.
Frequently Asked Questions
Why not build the entire board on RO4350B?
How much does a RO4350B + FR-4 hybrid actually save?
Can impedance be controlled reliably on a hybrid board?
Are hybrid boards less reliable than single-material boards?
What surface finish works best for hybrid RF boards?
Does XCE PCB build RO4350B + FR-4 hybrids with impedance control?
Planning a 4350B + FR-4 Hybrid Build?
Send us your Gerber files and requirements for a manufacturability review and a tailored quotation.
sales1@xcepcb.com
+86 180 3341 4657