
RO4350B runs on FR-4 equipment, yet production scrap still happens — and it clusters into five familiar failure families: delamination, hole-wall burrs, impedance drift, soldering thermal shock, and surface damage that cannot be polished away. Each has a root cause and a countermeasure. Here they are.
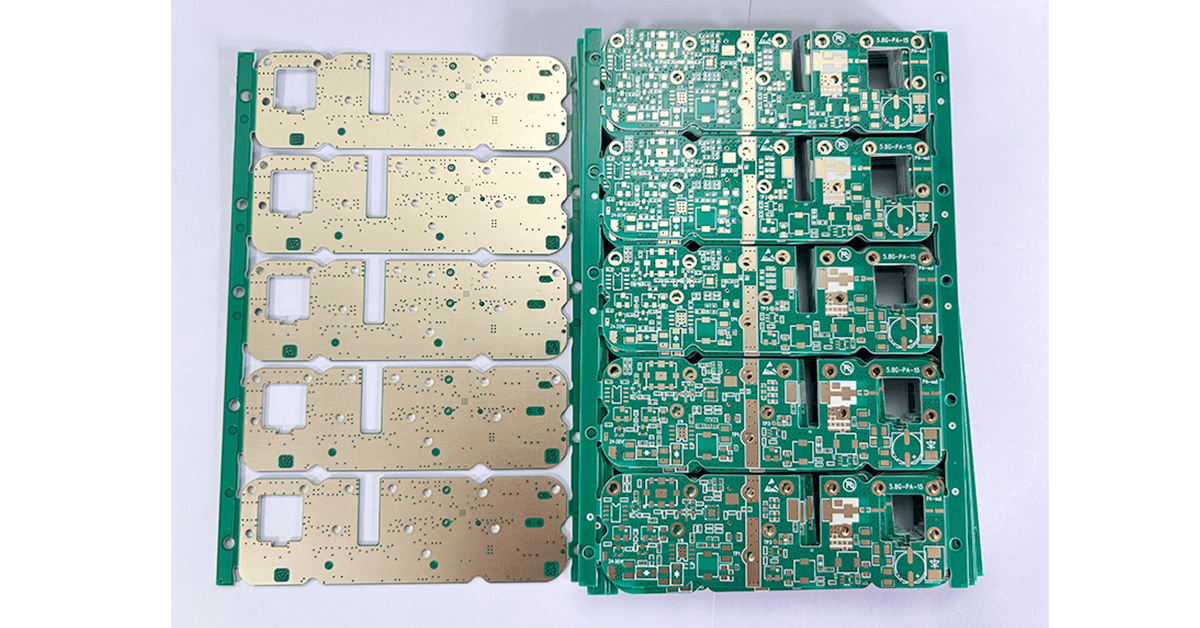
The Five Failure Families at a Glance
| Failure | Typical root cause | Core countermeasure |
|---|---|---|
| Interlayer delamination | Missing/incorrect surface treatment; moisture; uneven CTE stress | Permanganate desmear/browning + bake + stepwise press profile |
| Hole-wall burrs | Wrong entry/backup stack; dull bits | Hard composite entry with aluminum foil + sharp carbide |
| Impedance drift | Etch width error; Dk lot variation | Tight etch control + 100% laser inspection + TDR coupons |
| Soldering thermal shock | Peak temperature/dwell too high; bad profiles on metal-back | Optimized reflow profile; paste-print control on metal substrates |
| Surface contamination & damage | Bare-hand contact; mechanical grinding after etch | Gloves throughout; no mechanical rework — chemical only |
Failure 1: Interlayer Delamination
RO4350B is a hydrocarbon/ceramic thermoset — no PTFE activation needed, but the bond interface still demands chemical surface treatment. The standard approach is a permanganate-based desmear plus browning on copper, which roughens and conditions the surfaces for lamination adhesion. Skipping it, or running it with out-of-window chemistry, is the single most common cause of interlayer delamination.
Two aggravating factors compound it. First, absorbed moisture: panels exposed to humidity after opening flash to vapor during lamination or reflow — a bake of roughly 150 °C for 2 hours removes it. Second, thermal-expansion stress: multilayer boards with dense ground-via fields or blind/buried via structures see concentrated Z-axis expansion during reflow. The Z-CTE of RO4350B is 32 ppm/°C — better than FR-4’s typical 50–70, but a dense via field still concentrates the stress. Press profiles fight back: stepwise pressurization, slow heating and cooling at roughly 1–2 °C per minute, and full vacuum to minimize entrapped air.
The positive-side process flow that prevents these failures is detailed in our RO4350B manufacturing process guide.
Failure 2: Drilling Burrs and Hole-Wall Quality
RO4350B is hard and drills well with mechanical tooling, but “drills like FR-4” does not mean “drill carelessly.” Improper entry and backup materials — especially not using the recommended hard composite entry board with aluminum foil — leave burrs at hole entry. Burrs roughen the hole wall and set up plating defects: thin copper in the barrel, adhesion gaps, later barrel cracking under thermal stress.
The fix stack: sharp tungsten-carbide bits (ceramic filler abrades tools faster than epoxy), the correct entry/backup stack, and controlled hit counts per tool. Desmear after drilling guarantees a chemically clean wall before electroless copper.
Failure 3: Impedance Drift
Impedance on an RF board is set by dielectric thickness, etched line width, copper weight and solder-mask thickness. Two production variables dominate drift:
- Etching error. Millimeter-wave builds need line width held to roughly ±0.02 mm. High-precision tooling — electroformed stencils in imaging, tuned etch chemistry — plus 100% post-etch inspection with a laser diameter gauge keeps the process in control.
- Dk batch variation. RO4350B’s Dk is controlled to 3.48 ± 0.05 (about ±1.4%). That is tight for a laminate, but a design relying on exact impedance still sees it: the countermeasure is measuring the actual panel, not assuming the nominal. TDR coupons on the production panel close the gap.
XCE PCB controls impedance to ±10% with TDR coupon verification on every production panel.
Failure 4: Soldering and Thermal Shock Risks
Three distinct symptoms share one family:
- Substrate yellowing after soldering — peak temperature too high or dwell too long. Usually cosmetic, but it flags a profile problem that can progress to real damage on the next cycle.
- Fine-trace lift-off — traces around 4 mil (0.1 mm) detach when post-soldering thermal stress concentrates on narrow copper. Wider clearances, balanced copper distribution and honest reflow profiles prevent it.
- Bubbles on metal-backed assemblies — soldering RO4350B onto a metal (e.g., copper) substrate without a controlled temperature profile traps voids at the interface, degrading both heat transfer and mechanical strength. Solder-paste printing and reflow parameters need explicit engineering, not FR-4 defaults.
Failure 5: Surface Contamination and Irreparable Damage
The RO4350B laminate surface has a production property that surprises FR-4 veterans: it cannot be mechanically polished after etching. Marks from improper panel contact, or fingerprints from bare-hand handling, are effectively permanent — rework is limited to mild chemical cleaning (acid wash), which cannot recover deep contamination.
The countermeasure is procedural, not technical: operators wear clean gloves from cutting through final packing, bare-hand contact is prohibited, and finished-pattern boards are never mechanically ground or abraded at any stage.
Surface Finishes: What Lowers Loss and What Adds It
For RF performance, prioritize low-loss finishes: electroless silver is the low-conductor-loss choice, and electroplated gold works for durability-critical areas such as gold fingers (gold thickness to spec, typically ≥3 µin on the wearing surface). Avoid HASL — its uneven, rough surface adds conductor loss exactly where RF budgets can least afford it. ENIG remains the general-purpose default with black-pad quality control; the nickel-layer loss physics are quantified in our immersion-gold analysis.
How XCE PCB Prevents These Failures
XCE PCB builds RO4350B from 2 to 72 layers with permanganate desmear + browning as standard, stepwise press profiles under vacuum, hard-composite entry drilling, TDR coupons on every panel, and glove-line handling throughout — samples in as fast as 24 hours when laminate is in stock. For how hybrid RO4350B + FR-4 stacks change the failure picture, see the hybrid lamination analysis; for material selection against 4003C, the 4350B vs 4003C comparison.
Frequently Asked Questions
Why do RO4350B boards delaminate during reflow?
How do you prevent burrs when drilling RO4350B?
What causes impedance deviation in RO4350B production?
Why can't RO4350B surfaces be reworked mechanically?
Is HASL an acceptable finish for RO4350B RF boards?
Build RO4350B Without the Scrap Rate
Send us your Gerber files and requirements for a manufacturability review and a tailored quotation.
sales1@xcepcb.com
+86 180 3341 4657