
A stack-up is not a layer count with material names attached. It is the set of numbers — Dk, dielectric height, copper weight — that every impedance, every via and every thermal path on the board is calculated from. Get the sequence right and the rest of the design has somewhere to stand; get it wrong and no amount of routing skill recovers it. These are the eight steps we use, in the order that avoids rework.
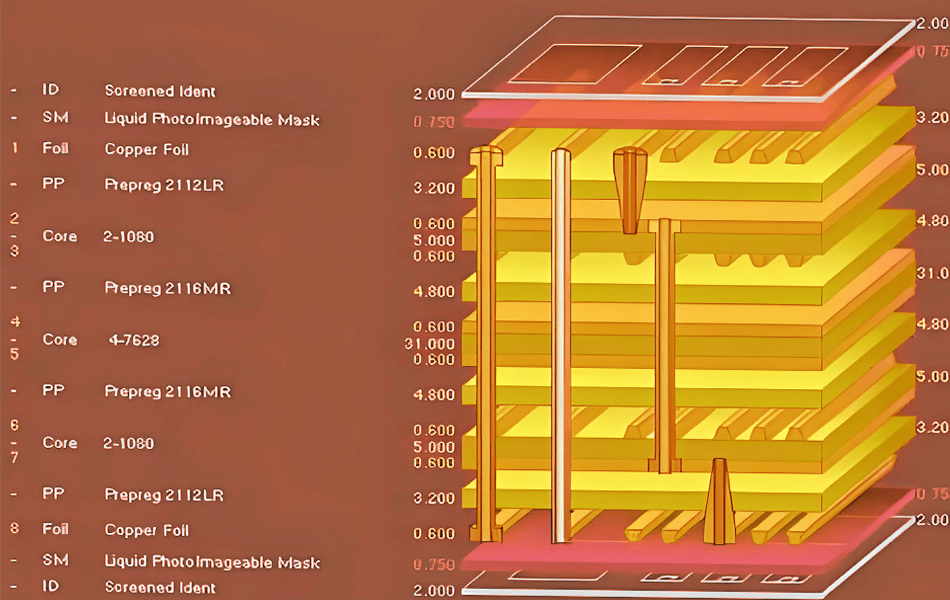
What a Stack-Up Actually Decides
Three numbers per dielectric layer, one rule across all of them, and one mechanical constraint. That is the whole subject:
- Dk — which value, and at which frequency. Every width on the board follows from it.
- Dielectric height — the h that impedance is calculated against, after pressing, not the catalogue nominal.
- Copper weight — part of the conductor loss, part of the width correction, and part of the balance that keeps the board flat.
- The rule — every signal layer has a continuous reference plane directly adjacent to it, and no RF trace crosses a split in that plane.
- The constraint — a symmetric build, because on PTFE the Z axis expands at 200 ppm/°C and above.
Everything else — layer numbering, material brand, whether the RF sits outside or inside — follows from these. The design decisions that precede the stack-up (loss budget, laminate choice, Dk basis) are set out in the high-frequency design steps guide; this article starts where that one ends.
Step 1 — Count Layers From Reference Planes, Not From Signals
The usual method — count the signal layers you think you need and add one ground — produces stacks that work on paper and fail in EMC. Count the other way: each signal layer needs a plane, and a stripline layer needs two.
The arithmetic is simple and unforgiving. With n routing layers all on stripline, you need n+1 planes. Four routing layers with two of them on microstrip (outer layers, each referenced to an inner plane) need three planes. This is why a real RF board usually lands on 6 or 8 layers for a circuit that a digital designer would do in 4: the planes, not the routing, set the count.
Two consequences are worth stating because they are routinely missed. A two-layer board has no stripline option at all — impedance control is limited to coplanar waveguide or to microstrip over the full board thickness, which forces very wide traces and a poor return path. And a four-layer board with one ground and one power plane gives you exactly two controlled-impedance signal layers, both microstrip, both on the outside; the inner pair cannot carry controlled-impedance routing without losing its reference.
Step 2 — Place the RF Layers: Outside, Inside, or Both
This single decision changes the width of every RF trace, the isolation between channels, and how easy the board is to tune.
| Outer layer (microstrip) | Inner layer (stripline) | |
|---|---|---|
| Isolation between RF chains | Moderate — one ground reference, field partly in air | Better — enclosed by planes above and below |
| Trace width for 50 Ω | Wide (0.56 mm at h = 0.254 mm on RO4350B) | Narrow (0.23 mm at b = 0.508 mm) |
| Etch sensitivity | ±2.8% impedance for ±25 µm | ±6.8% for the same ±25 µm |
| Tuning and rework | Easy — stubs and trims are accessible | Difficult — buried |
| Finish / mask effects | Direct: ENIG nickel and mask both act on the line | None on the RF line itself |
| Typical use | Antennas, filters, anything trimmed after first article | High-isolation chains, delay-matched runs, dense arrays |
The width difference is larger than most designers expect, and it is purely geometric. For the same total dielectric between planes, a stripline centre conductor is roughly 2.5× narrower than the equivalent microstrip. Narrower means the same etch tolerance is a larger fraction of the width — which is where the second row of that table comes from. If a design needs both stripline isolation and a tight impedance window, the dielectric has to be thicker, and thicker dielectric means fewer layers in the same board thickness. The stack-up is always a negotiation between those three.
Step 3 — Assign the Stack With a Purpose for Every Layer
Three templates cover most high-frequency work. Leave every layer unnamed and someone will route a clock through the middle of an RF reference.
| Layers | Stack | Where it fits | Weak point |
|---|---|---|---|
| 4 | L1 RF microstrip · L2 GND · L3 PWR · L4 RF microstrip | Single RF chain, moderate density, cost sensitive | L4 references L3 (power) — needs solid decoupling to behave as RF ground |
| 6 | L1 RF microstrip · L2 GND · L3 RF stripline · L4 GND · L5 PWR · L6 mixed | Two RF environments: trimmable outside, isolated inside | Asymmetric plane distribution — check the build balance, not just the electrical symmetry |
| 8 | L1 RF · L2 GND · L3 RF stripline · L4 GND/PWR · L5 PWR/GND · L6 RF stripline · L7 GND · L8 RF | Phased arrays, multiple chains, delay matching | Thickness — 8 layers of PTFE is a Z-CTE and aspect-ratio problem as much as an electrical one |
Two habits matter more than the template. First, keep the RF reference planes solid — a plane that carries a few digital signals is no longer a reference, and the RF return current will find the gaps. Second, put the power plane next to a ground plane, not next to an RF layer: the power-ground pair is a decoupling capacitor, and the RF layer does not benefit from being sandwiched against it.
Step 4 — Fix the Electrical Thickness, Not the Nominal Thickness
Impedance is calculated against the dielectric height after lamination. Three things move that number away from the catalogue value:
- Bonding layers count. A 0.508 mm core plus a 0.1 mm bondply is 0.608 mm of dielectric, not 0.508. On PTFE the bond line is usually a FEP or modified-PTFE film and holds its thickness; on thermoset stacks prepreg flows and thins under pressure. Either way, the value that goes into the field solver is the pressed value agreed with the fabricator.
- Copper thickness eats into the gap. A 1 oz inner layer is 35 µm per side; on a 0.1 mm dielectric that is a third of the gap before any resin flow.
- Dk depends on thickness and frequency. On 0.101 mm RO4350B the specified process Dk is 3.36, not 3.48, and the wideband design value is 3.66. The stack note has to say which one the widths were calculated with, or the next engineer will re-derive them differently.
For mixed stacks there is a fourth: the adhesive at the hybrid interface. A 0.1 mm bondply of a different Dk in series with the RF dielectric shifts the effective Dk of the whole gap, and that shift belongs in the model — it is one of the reasons hybrid builds are harder to hit inside ±10% than single-material ones.
Step 5 — Build Symmetrically, and Balance the Copper
Symmetric means mirror image about the centre line: same dielectric thickness, same copper weight, same material class on both halves. On a laminate that expands 200 ppm/°C in Z, an unbalanced stack bows during cool-down from the press, and the bow is permanent. The barrel damage shows up later, as a cracked plating after thermal cycling rather than as a failing electrical test.
| Laminate | CTE X / Y | CTE Z | Z relative to copper (17) |
|---|---|---|---|
| RO4350B | 10 / 12 | 32 | 1.9× |
| RO4003C | 11 / 14 | 46 | 2.7× |
| RO3010 | 13 / 11 | 16 | <1× — below copper |
| Taconic TLY-5 | 26 / 15 | 217 | 12.8× |
| RT/duroid 5880 | 31 / 48 | 237 | 14× |
Note what the table makes obvious: on PTFE the idea of “matching CTE to copper” is not achievable in Z — you cannot match a 13× difference, you can only decide who absorbs it. That is why the stack rules for PTFE are symmetry, aspect ratio at or below 6:1 on critical vias, and high-ductility plating rather than a CTE match. In X and Y the situation is the opposite and benign: RO4350B’s 10/12 sits below copper’s 17, which is good for layer-to-layer registration.
Copper balance is the second half of the same problem. A layer that is 80% copper facing a layer that is 20% copper will warp regardless of dielectric symmetry, and on thin cores it can also distort the pressed thickness locally — which shows up as an impedance map rather than a single value.
Step 6 — Put the FR-4 Where It Costs Least
Most cost-controlled RF boards are hybrids: high-frequency laminate on the layers that carry RF, FR-4 in the middle. The rule that decides whether it works is that the RF laminate goes on the outside of the stack, one core per RF layer, with the FR-4 core in the centre so the build stays mechanically symmetric.
Three things then have to be right. The interface prepreg must be compatible with both resin systems — on RO4000 series that means the manufacturer’s own bonding ply or a high-Tg FR-4 prepreg rated for the press cycle. The CTE mismatch at the interface has to be absorbed by the plated barrels, which is where ductility specifications come from. And the total dielectric height under each RF line must include the FR-4 side if the reference is an inner plane. The process detail is in the hybrid lamination analysis, and the material choice between RO4350B and RO4003C in the 4350B versus 4003C comparison.
Where the RF laminate is PTFE rather than thermoset, the same hybrid becomes a different process: PTFE does not flow, so bonding relies on FEP film or low-flow prepreg, and hole-wall activation needs plasma or sodium naphthalene. That path is covered in the 5880 and FR-4 lamination guide.
Step 7 — Design the Thermal Path in the Stack, Not Around It
High-frequency laminates are thermal insulators by electronic standards: RO4350B conducts 0.69 W/m·K, RO3003 0.50, RT/duroid 5880 and TLY-5 around 0.20–0.22, against roughly 400 for copper. Adding a “thermal layer” of high-conductivity material inside an RF stack therefore does two things at once: it barely helps, because the heat still has to cross the low-conductivity RF dielectric, and it changes the electrical environment of every layer above it.
What works is vertical. A power amplifier gets a thermal pad on the top copper, a field of plugged thermal vias directly beneath it (0.3–0.5 mm drill on roughly 0.8–1.0 mm pitch), and a solid copper area on the bottom or on an internal plane connected to a heat spreader or metal backplane. The vias are the thermal path; the planes are the spreading; the laminate is only the gap that has to be crossed.
The electrical caveat matters as much: thermal vias under an RF line are a periodic discontinuity, and a via field that reaches under a matching network will shift it. Keep the thermal field under the device and its DC feed, and clear of any tuned RF trace.
Step 8 — Verify With a Solver, Then Freeze It With a Coupon
Run the stack through a 2D field solver for every line type on the board and record the resulting geometry — not just the impedance target. What must be in the model: design Dk for the band in use, pressed dielectric heights including bondply, copper thickness, solder mask on outer layers, and a roughness-aware conductor model if any RF path is long at millimetre-wave frequency.
Then freeze it. A stack-up is only real once a coupon on the production panel has measured it by TDR and the result has been accepted against a written band. Two practical notes from production: the coupon has to use the same line type and reference distance as the product (a convenient 50 Ω microstrip coupon does not validate a stripline layer), and any stack change — a substituted prepreg, a different core thickness — invalidates the coupon and needs a re-measure, not an email.
XCE PCB builds these stacks on Rogers, Taconic and F4B laminate with impedance coupons on every RF lot: 2–72 layers, ±10% impedance, panels to 600 × 1200 mm for large array boards, 5,000 m² of production space and 80+ engineers, with samples in as fast as 24 hours so a stack can be measured before tooling is committed. For the fabrication sequence the stack feeds into, see the twelve-step manufacturing process.
Stack-Up Review Checklist
| Check | Pass condition | |
|---|---|---|
| 1 | Every signal layer has an adjacent solid plane | No signal layer references a plane that carries routing |
| 2 | No RF trace crosses a plane split | Checked on every layer transition, including connector fan-out |
| 3 | Build is symmetric about the centre | Same dielectric thickness and copper weight either side |
| 4 | Dk basis is stated | Design or process value named, with the frequency band |
| 5 | Pressed thicknesses, not catalogue | Bondply and copper included in the h used for impedance |
| 6 | Stripline width is achievable | Etch tolerance as a fraction of W is inside the impedance budget |
| 7 | Via aspect ratio | ≤8:1 general, ≤6:1 on PTFE with Z-CTE above 200 |
| 8 | Thermal path defined | Via field under each dissipating device, clear of tuned traces |
| 9 | Coupon agreed | Line type, reference distance, measurement method and band in writing |
A stack that passes all nine is one a fabricator can quote without qualification — and one whose impedance you can defend at incoming inspection with a measurement rather than an opinion.
Frequently Asked Questions
What are the main steps in high-frequency PCB stack-up design?
How many layers does a high-frequency board need?
Should RF traces be on the outer layers or buried?
Why does the stack-up need to be symmetric?
Does a thinner dielectric between signal and ground increase crosstalk?
Where should the FR-4 go in a hybrid high-frequency stack?
Need a Stack-Up Reviewed Before Release?
Send us your Gerber files and requirements for a manufacturability review and a tailored quotation.
sales1@xcepcb.com
+86 180 3341 4657