
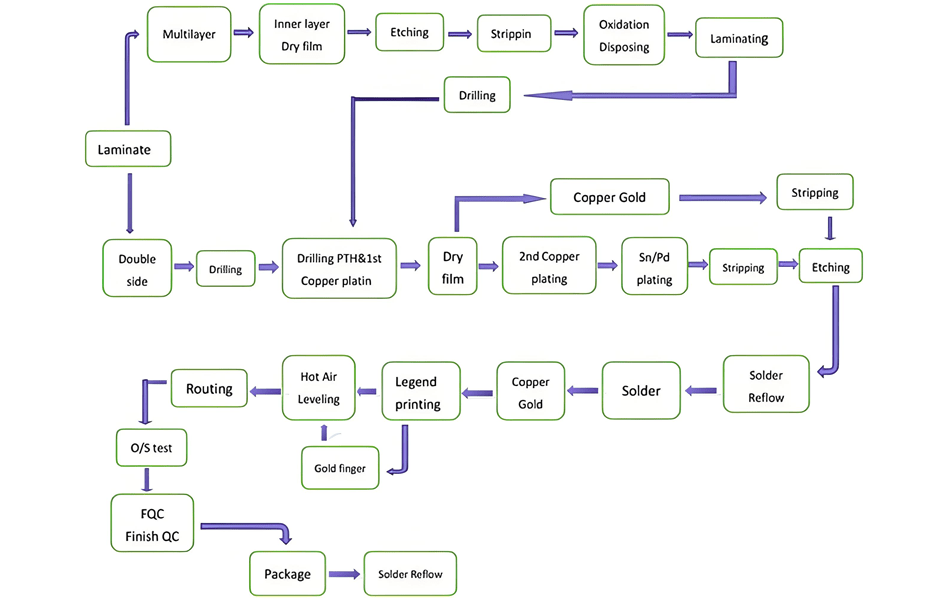
A high-frequency board runs through the same twelve process steps as any FR-4 board. What changes is five of them — and those five are where yield is won or lost. This is a process map for engineers and buyers: what each step controls, why the laminate forces a different setting, and the failure mode that appears when it is skipped. Deep dives on individual steps are linked where they exist.
Three Material Facts That Propagate Through the Whole Flow
Almost every process difference on a high-frequency board traces back to one of three properties of the laminate. Once you hold these three, the rest of the flow stops looking arbitrary.
- PTFE does not melt and flow. It is semi-crystalline with a melting point around 327 °C; it softens but never becomes a liquid that fills a void. There is therefore nothing to “squeeze out” during lamination — bonding has to come from an added adhesive layer, and trapped air has nowhere to go.
- The Z axis expands roughly ten times faster than copper. PTFE-class laminates sit at 200–240 ppm/°C against copper’s 17. Every plated barrel is a spring that has to absorb that difference over every thermal excursion the board will ever see.
- The dielectric is a poor conductor of heat and a good insulator of charge. Thermal conductivity around 0.22 W/m·K means heat moves through copper, not through the laminate — which changes how you drill, how you reflow and how you place vias.
Everything below is a consequence of these three, plus the low Df that the material exists for in the first place.
The Process Map
Twelve steps, in order, with the one parameter that decides whether the step succeeded and the difference a high-frequency laminate introduces. Steps 6, 7, 8, 9 and 11 are the five that materially change.
| # | Step | What is controlled | High-frequency difference | Failure mode if skipped |
|---|---|---|---|---|
| 1 | Design and RF simulation | Impedance targets, Dk model, loss budget | Must use design Dk, not the process Dk on the datasheet, and a coupon-verified model | Systematic impedance offset — every board in the lot is wrong the same way |
| 2 | Stackup | Layer assignment, dielectric thickness, symmetry | Symmetry is a reliability requirement, not a cosmetic one, because of the Z-CTE | Warp after press, layer-to-layer registration drift |
| 3 | Artwork and film output | Etch compensation, panelisation, tooling | On thin dielectric, etch compensation is a larger share of the width | Width off target → impedance out of band |
| 4 | Material cutting and bake | Panel size, grain orientation, moisture | Warp and weft are not equivalent (CTE 26 vs 15); orientation must be consistent between prototype and production | Anisotropic shrinkage, directional Dk shift |
| 5 | Inner-layer imaging and etch | Line width, undercut, registration | Soft resin needs gentler handling; scratches on the dielectric are permanent | Impedance drift, opens on fine features |
| 6 | Lamination | Temperature, pressure, ramp and cool rate | No resin flow: bonding via FEP film at 290–315 °C or low-flow prepreg at 180–190 °C | Delamination and voids — often only after thermal cycling |
| 7 | Drilling | Hole quality, position, burr | Soft resin plus abrasive glass narrows the parameter window | Rough or smeared walls → plating voids and barrel cracks |
| 8 | Desmear and hole-wall activation | Adhesion of electroless copper | Plasma or sodium-naphthalene required; permanganate alone will not activate PTFE | Plating adhesion failure — the classic PTFE scrap mode |
| 9 | Plating | Copper thickness and ductility | Z-CTE 217 demands high-ductility copper (≥20% elongation) and aspect ratio ≤8:1 | Barrel fracture after thermal cycling — passes at incoming, fails in the field |
| 10 | Outer-layer imaging and etch | Width, spacing, copper profile | Foil roughness now dominates conductor loss above ~20 GHz | Insertion loss above budget despite a correct laminate |
| 11 | Solder mask and surface finish | Mask adhesion, finish thickness, nickel barrier | PTFE’s low surface energy fights mask adhesion; nickel adds loss at mmWave | Mask blistering after reflow; unexplained loss at 30 GHz and above |
| 12 | Test and inspection | Coupon impedance, continuity, microsection | RF sample testing (S21/S11) belongs in acceptance, not in the customer’s lab | Latent failures shipped as “electrically good” |
Front End: Design, Stackup and Fabrication Data
The cheapest place to fix a high-frequency board is the data package. Two items decide most of what follows.
Design Dk versus process Dk. Datasheets list a process Dk measured on a test coupon; simulation needs the design Dk, which is usually slightly higher because it folds in the field distribution of a real transmission line. Mixing the two produces a systematic impedance offset that no amount of etch tuning will remove. State which value the design used, on the drawing, so the fabricator is not guessing.
Coupon definition. A controlled-impedance coupon on the production panel, measured by TDR, is the only way to close the loop. ±10% is the working acceptance band; on thin dielectric (≤0.2 mm) the same band is much harder to hold because etch variation becomes a first-order term. Say so on the drawing rather than discovering it at first article.
Two smaller front-end items are worth writing down as well: grain orientation (warp and weft differ) and the requirement that the prototype and production panels come from the same orientation, otherwise the first article is not a valid predictor.
Material Prep, Imaging and Inner-Layer Etch
Cutting and baking look like housekeeping and behave like process control. PTFE laminates arrive with residual moisture and internal stress from the press; a bake before inner-layer processing reduces dimensional movement later, and consistent panel orientation keeps anisotropic shrinkage predictable.
Imaging itself is conventional — dry film, expose, develop, etch — with one handling caveat: the dielectric surface is soft, and a scratch or a burr rolled into the surface is not repairable. Tooling, transport and stacking discipline matter more than they do on FR-4.
Etch compensation is where the electrical consequence sits. Since Dk is low (2.2), 50 Ω lines are wide — around 0.84 mm on 0.254 mm dielectric — which is forgiving. On 0.127 mm dielectric the line is only 0.44 mm and a ±25 µm etch window is already ±5% of the width. The thinner the core, the more the etcher, not the designer, sets the impedance.
Lamination: Where PTFE Builds Are Won or Lost
This is the step that separates a fabricator who has a PTFE line from one who has read about PTFE. Because the resin does not flow, there is no mechanism to fill voids or displace air. Bonding must come from an interlayer:
- FEP or modified-PTFE film, pressed around 290–315 °C. This is the route that gets quoted as “a 300 °C press cycle”. It delivers the best dielectric result because the bond line is itself low loss, and it demands a slow ramp and a slow cool.
- Low-flow prepreg at 180–190 °C, which is easier on tooling and suits hybrid stacks with FR-4, at some cost in dielectric performance at the bond line.
Three controls decide the outcome: vacuum and dwell (air is the enemy, and there is no resin flow to expel it), ramp and cool rate (the Z-CTE of 217 is generating stress the entire time the stack is hot, so a fast cool locks that stress in), and stack symmetry (copper balance and dielectric balance above and below the centre line, otherwise the panel bows and registration drifts).
The failure signature to watch for is a bond that looks and tests fine at incoming and delaminates after two or three thermal cycles. That is why first-article acceptance for a PTFE build should include a thermal cycle before sign-off, not just a microsection. The hybrid version of this problem — PTFE against FR-4 — is worked through in the hybrid lamination technology analysis.
Drilling and Hole-Wall Preparation
Two properties fight each other at the drill: the resin is soft (it smears) and the reinforcement is abrasive glass (it dulls tooling fast). A dull bit in soft resin produces a torn wall; a fast feed in glass produces a rough one. The working window is narrower than on FR-4, which means drill parameters should be qualified per stackup rather than copied from a standard recipe.
The common statement that holes must be burr-free “to minimise high-frequency signal loss” is a category error worth correcting. Burrs and wall roughness affect plating coverage and barrel integrity — they cause voids, weak welds and ultimately cracked barrels. Insertion loss is set by the transmission line, not by the via wall; a rough via does change its impedance slightly, but the reason to control it is reliability. Practical acceptance: burr at or below 0.025 mm, and a wall quality confirmed by microsection.
Then the step that decides PTFE yield: desmear and activation. Permanganate, the standard FR-4 desmear, does not attack PTFE. Specify plasma treatment (O2/CF4) or sodium-naphthalene before electroless copper, and verify with a hole-wall microsection plus a thermal-stress test. A shop that skips this step will still ship boards that pass electrical test — and fail in the field.
Plating, Outer Layers and Copper Profile
Plating thickness is the usual acceptance criterion, and on a PTFE build it is the wrong one on its own. What matters is ductility: with Z-CTE at 217 ppm/°C, the barrel has to stretch several percent over a thermal excursion, and brittle copper cracks before it stretches. Specify high-ductility plating (≥20% elongation), keep the aspect ratio at or below 8:1, and treat corner microsections as mandatory.
On the outer layers, two effects move the loss number without touching the laminate:
- Copper foil profile. Above roughly 20 GHz, current crowds into the surface and roughness adds conductor loss. Very-low-profile foil is not marketing — on a material whose dielectric loss is already minimal, the foil becomes the dominant loss term.
- Etch tolerance. Width error translates directly into impedance error, and the effect is amplified on thin dielectric. This is why the coupon, not the etcher’s experience, has to be the referee.
The material side of this trade — matching copper weight and foil type to the current the design actually carries — is covered in the copper thickness guide.
Solder Mask, Surface Finish, and an Error That Keeps Being Copied
PTFE has low surface energy, so solder mask adhesion is a real problem rather than a theoretical one. Expect to need plasma pre-treatment before mask, to accept that mask over PTFE is a mechanical attachment rather than a chemical bond, and to consider leaving the mask off antenna and matching sections entirely — which improves both loss and reliability.
Surface finish is where a widely copied paragraph is simply inverted. The claim is that ENIG gives the lowest loss and that immersion silver loses slightly more. At microwave and millimetre-wave frequencies the physics runs the other way:
| Finish | Loss behaviour | Where it belongs |
|---|---|---|
| Immersion silver | Lowest loss — silver directly on copper, no barrier layer | mmWave and low-loss RF paths; short shelf life, needs good packaging |
| OSP | Very low loss (organic, thin) | High-volume consumer RF with a controlled assembly window |
| ENIG | Nickel layer (3–6 µm) has roughly a quarter of copper’s conductivity and sits exactly where the current flows above ~10–30 GHz | Fine-pitch, long-life, gold-wire or aluminium-wire assembly; acceptable when traces are short |
| ENEPIG / hard gold | Higher loss, best wear and bondability | Edge connectors, gold ball bonding, harsh environments |
So ENIG is the right answer for durability, fine pitch and assembly yield — not for minimum insertion loss. The rule that works in practice: below 30 GHz ENIG is everywhere and nobody notices; above 30 GHz, check it line by line, and use silver on the long paths. That trade, including the nickel barrier and IPC-4552 thickness control, is examined in the immersion-gold analysis.
Test, Inspection and What “Accepted” Should Mean
Electrical test proves continuity. On a high-frequency board that is a floor, not an acceptance criterion. Four checks belong in the acceptance package:
- Impedance coupon by TDR, per lot, against the ±10% band — and measured on the same panel, not on a separate test vehicle from another press cycle.
- RF sample measurement: S21 and S11 on a representative structure, so the customer is not the first to discover a loss problem.
- Microsection: hole wall, plating thickness and ductility, dielectric thickness, and corner locations rather than the middle of the panel.
- Thermal stress or cycling before first-article sign-off — the step that catches the lamination and plating problems that pass at room temperature.
XCE PCB runs this flow on a PTFE-capable line: plasma and sodium-naphthalene desmear in house, controlled-impedance coupons on every RF lot, 2–72 layers, impedance ±10%, panels to 600 × 1200 mm, and samples in as fast as 24 hours with Rogers, Taconic and F4B laminate in stock. For the step-by-step owner’s view of the same flow on one specific material, see the RO4350B manufacturing walkthrough; for the general production pitfalls and how they are usually caused, the production key points guide and the core production issues analysis.
Frequently Asked Questions
What are the main steps in high-frequency PCB manufacturing?
Why is lamination different for PTFE laminates?
Is ENIG the lowest-loss surface finish?
Which desmear process is required for high-frequency boards?
How is impedance controlled during production?
What plating specification matters most for PTFE builds?
Reviewing a High-Frequency Process Flow?
Send us your Gerber files and requirements for a manufacturability review and a tailored quotation.
sales1@xcepcb.com
+86 180 3341 4657