
Solder mask is specified as a protective coating, and it is bought as a coating: colour, gloss, thickness, cure. Electrically it is something else. Twenty-five micrometres of a material with a dielectric constant near 3.8 sits directly on top of every trace, and how much that matters depends entirely on what is underneath it — on 0.127 mm PTFE it can move a 50 Ω line by six per cent, on 0.508 mm laminate barely two. Getting this right is a two-line decision in the stack-up, or a whole lot of re-tuning after the first impedance coupon.
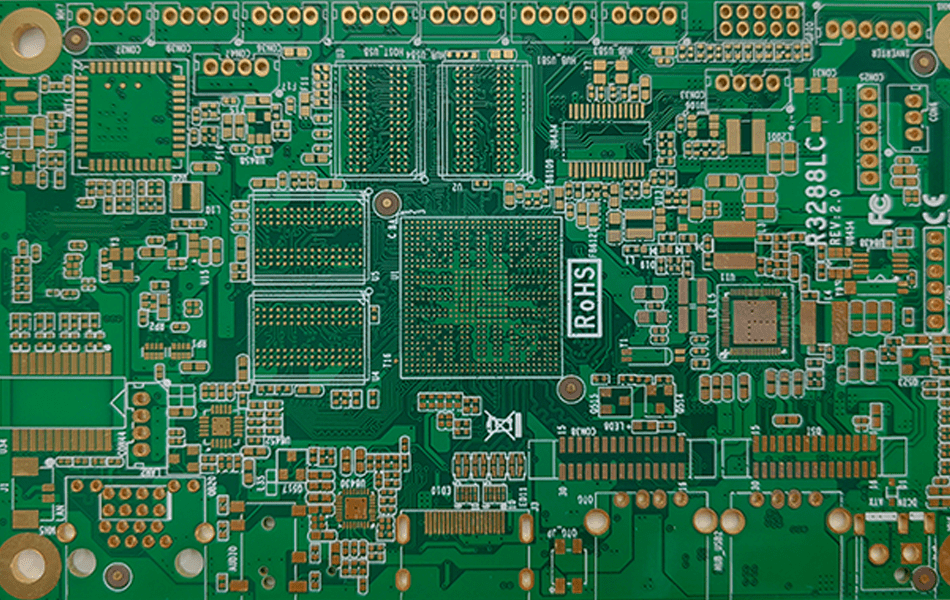
Two Specifications Wearing One Name
Every solder mask is described by the same two lines in a purchase order: a colour and a standard. That covers the protective function — solder containment, insulation, marking, and protection from handling and contamination — and says nothing about the electrical one.
Electrically, the mask is a thin dielectric covering the whole board. Over a microstrip it changes the effective dielectric constant of the field above the trace; between traces it adds a leakage path with its own loss tangent; over a launch or a filter it detunes what was simulated in air. All three effects scale with thickness over dielectric height, which is why the same mask process is harmless on one build and significant on another.
This is the step after plating in the twelve-step sequence, and the impedance budget it consumes is part of the same calculation set out in the design step guide.
The Numbers, Since None Are Usually Quoted
| Property | Typical value for liquid photoimageable mask | Why it matters |
|---|---|---|
| Thickness over a trace | 15–25 µm | Sets how much of the field above the trace is in mask |
| Dielectric constant | 3.5–4.2 at 1 MHz | 1.7× a PTFE substrate; 0.9× an FR-4 one |
| Loss tangent | 0.02–0.03 | Twenty to thirty times the Df of 5880 |
| Colour | Any | Pigment changes nothing electrically at RF |
| Final cure | ≈150 °C, 60 min | Below the PTFE service range; safe on all families |
The dielectric constant row is where high-frequency work differs from the general case. On FR-4 at Dk 4.3 a 3.8 mask is slightly lower than the substrate, so covering a trace barely changes the field. On 5880 at Dk 2.20 the same mask is 1.7 times the substrate, so the field above the trace is suddenly in a much denser dielectric.
What 25 µm of Mask Does to Impedance
The effect is a first-order calculation, and the useful part is the trend rather than the third digit. Treating the mask as an additional capacitance over the trace, the shift in effective Dk is roughly proportional to (Dkmask − 1) × t / h. Thickness over height, not thickness alone.
| Build (25 µm mask, Dk 3.8) | t / h | 50 Ω line before | After mask | Shift |
|---|---|---|---|---|
| 5880, 0.127 mm | 0.20 | 50.0 Ω | 46.7 Ω | −3.3 Ω (−6.6%) |
| 5880, 0.254 mm | 0.10 | 50.0 Ω | 48.3 Ω | −1.7 Ω (−3.5%) |
| 5880, 0.508 mm | 0.05 | 50.0 Ω | 49.1 Ω | −0.9 Ω (−1.8%) |
| 4350B, 0.254 mm | 0.10 | 50.0 Ω | 48.8 Ω | −1.2 Ω (−2.3%) |
| 4350B, 0.508 mm | 0.05 | 50.0 Ω | 49.4 Ω | −0.6 Ω (−1.2%) |
Three practical readings. A thin PTFE build with mask over the RF lines can spend a third of a ±10% budget on the mask alone. A modest 0.508 mm build spends almost nothing. And the direction is always the same — the mask lowers impedance — so a coupon measured before mask reads high, which is exactly the discrepancy that shows up between a fabricator’s in-process coupon and the customer’s final measurement.
The design answers are all cheap: widen the trace by the calculated amount, open the mask over the RF line (mask-defined keep-out, common on filter and antenna structures), or specify the mask thickness in the stack-up so the coupon is measured on the finished article. The expensive answer is discovering it after the first lot.
Step 1 — Preparation, and the PTFE Adhesion Problem
Cleaning is routine: remove oxide, contamination and resist residue, then dry. The step that is not routine is adhesion promotion, and on PTFE it is the whole battle.
Surface energy is the number behind it. FR-4 sits around 40 mN/m, which most liquid masks wet readily. PTFE is one of the lowest-energy surfaces in engineering, in the high teens to about 20 mN/m, so a mask that cures perfectly well on FR-4 will form a film on PTFE that looks correct, passes a visual inspection, and lifts at the edge of a large copper pour after the first reflow or the first mechanical shock.
Three approaches are used, in increasing order of reliability. A plasma treatment before coating, which raises surface energy and adds polar groups. An adhesion promoter designed for fluoropolymers, applied as a thin primer. Or keeping the mask off the fluoropolymer altogether where the geometry allows — which is often the honest answer on an RF board, where large areas of 5880 are better left bare with a defined finish than covered with a film that may peel.
Step 2 — Coating: Screen, Spray or Curtain
Liquid photoimageable mask is applied by screen printing, spray coating or curtain coating. The choice is made on geometry and volume, and it determines the thickness distribution that the impedance calculation above assumed.
| Method | Thickness control | Best for | Weakness |
|---|---|---|---|
| Screen printing | Good, defined by mesh and emulsion | High volume, flat boards | Thin over tall features; mesh marks |
| Spray coating | Moderate, program dependent | Mixed heights, prototypes | Overspray, edge build-up |
| Curtain coating | Very uniform on flat panels | Fine-line, high layer count | Needs a flat panel; waste at start-up |
What matters for RF is thickness over the trace, not average thickness on the panel. Mask thins over the top of a trace and pools in the gaps beside it, so a process that measures 20 µm on a coupon may be 12 µm on a 35 µm-high trace and 30 µm in the trench next to it. That is one more reason the impedance effect is measured, not assumed.
Step 3 — Tack Dry, Exposure and the Resolution Limit
Tack dry drives the solvent out so the film can be handled and exposed without sticking to the artwork. Typical conditions are 70–80 °C for a period set by the coating weight, and the control point is the residual solvent: under-dried film sticks and marks; over-dried film does not develop cleanly and leaves scum in the openings.
Exposure cross-links the film through a phototool or by direct imaging. The resolution limit is what sets the design rules: a solder dam between two pads needs a finite width to survive development and to stay put through reflow, and 0.10–0.15 mm is the practical range for production. Below that the dam is defined but fragile, and it fails as a bridged solder joint rather than as a mask defect.
Registration to the copper is the second-half of the tolerance. The mask opening is normally 0.05–0.1 mm larger than the pad per side, which protects the pad from mask encroachment at the cost of a smaller dam. On a fine-pitch device the two requirements — opening big enough, dam wide enough — can be mutually exclusive, and that is a design decision, not a process one.
Step 4 — Development and Cure
Development removes the unexposed film in a dilute alkaline solution, typically around 1% sodium carbonate, at a controlled temperature and conveyor speed. Under-development leaves a scum in the openings that blocks wetting and causes poor solder joints; over-development attacks the dam edges and lifts resist at the interface with copper.
Final cure is a bake, usually around 150 °C for 30–60 minutes, which completes the cross-linking and drives adhesion. This is the step where an under-cured mask reveals itself later: it passes a tape test when new and fails after a reflow cycle, because the cure that was missing is the one that survives thermal excursion.
On high-frequency laminate, cure temperature is not the constraint — 150 °C is inside the service range of every family discussed here, including PTFE. What is a constraint is the number of thermal excursions: each reflow adds a cycle to a mask on a low-surface-energy substrate, and a mask that is marginal on adhesion degrades with each one.
Step 5 — Loss, Not Just Impedance
A mask with a loss tangent of 0.02–0.03 is not a neutral covering at millimetre wave. Only the fringing field above the trace passes through it, so the contribution is a fraction of the total loss — but on a 5880 line whose dielectric loss is already at the floor, that fraction can dominate the difference between two otherwise identical boards.
The practical consequence is that the loss figure quoted for a laminate is measured on bare material, and the board that ships has mask over it. If a link budget was built on the datasheet number, the mask is one of the items that was not in it — along with copper roughness and finish, as set out in the plating step.
Where Solder Mask Goes Wrong
| Symptom | Root cause in this step | Fix |
|---|---|---|
| Mask lifts at the edge of a copper pour on PTFE | Surface energy never raised; no plasma or primer | Plasma or fluoropolymer promoter; or leave the area bare |
| Impedance 2–3 Ω low on a thin PTFE build | Mask thickness not in the model (t/h high) | Widen the trace, open the mask, or model it |
| Coupon reads 50 Ω, customer measures 48 | Coupon measured before masking | Measure after cure, on the finished article |
| Scum in mask openings, poor solder wetting | Under-exposure or over-dried film | Exposure energy step test; control tack dry by weight |
| Mask bridges between fine-pitch pads | Dam narrower than the process can hold | 0.10–0.15 mm minimum dam, or mask-defined pads |
| Loss higher than the laminate datasheet predicts | Mask Df 20–30× the substrate over the RF line | Open the mask over RF; re-run the link budget |
Solder Mask Checklist
| # | Check | Pass condition |
|---|---|---|
| 1 | Mask Dk and thickness recorded | 3.5–4.2 and 15–25 µm, used in the model |
| 2 | t/h checked for thin builds | ≤0.10, or the trace widened to compensate |
| 3 | RF lines mask-open where loss matters | Defined in the data package, not decided in the shop |
| 4 | Surface energy raised on PTFE | Plasma or promoter before coating |
| 5 | Coating method matched to topography | Curtain or spray for mixed heights |
| 6 | Tack dry controlled by residual solvent | No stick, no scum |
| 7 | Dam width within process capability | 0.10–0.15 mm minimum |
| 8 | Opening 0.05–0.1 mm per side over pad | No encroachment, no exposed trace |
| 9 | Final cure verified | ≈150 °C, 30–60 min, tape test after reflow |
| 10 | Impedance coupon measured after mask | Finished-article value inside ±10% |
Conclusion
Solder mask is bought as a coating and behaves as a dielectric. On a high-frequency board the two facts that decide whether it is harmless are the ratio of mask Dk to substrate Dk and the ratio of mask thickness to dielectric height — which is why the same process is a non-event on 0.508 mm 4350B and a 6% impedance shift on 0.127 mm PTFE.
The claims worth discarding are that mask is electrically neutral at RF (it is not, in either Dk or Df), that a mask that adheres to FR-4 will adhere to PTFE (surface energy differs by a factor of two), and that impedance is settled at the coupon stage (a coupon measured before cure is measured before the mask is in the stack).
XCE PCB applies liquid photoimageable mask with plasma preparation on fluoropolymer, mask-open RF lines where the loss budget needs them, and impedance coupons measured after final cure: 2–72 layers, impedance ±10%, panels to 600 × 1200 mm, 5,000 m² of production space and 80+ engineers, with samples in as fast as 24 hours.
Frequently Asked Questions
Does solder mask affect impedance?
How thick is solder mask?
Why does solder mask peel off PTFE?
Should RF traces be covered with mask?
Why does my coupon read 50 Ω but the finished board 48 Ω?
What is the minimum solder dam width?
Need Mask That Does Not Move Impedance?
Send us your Gerber files and requirements for a manufacturability review and a tailored quotation.
sales1@xcepcb.com
+86 180 3341 4657