
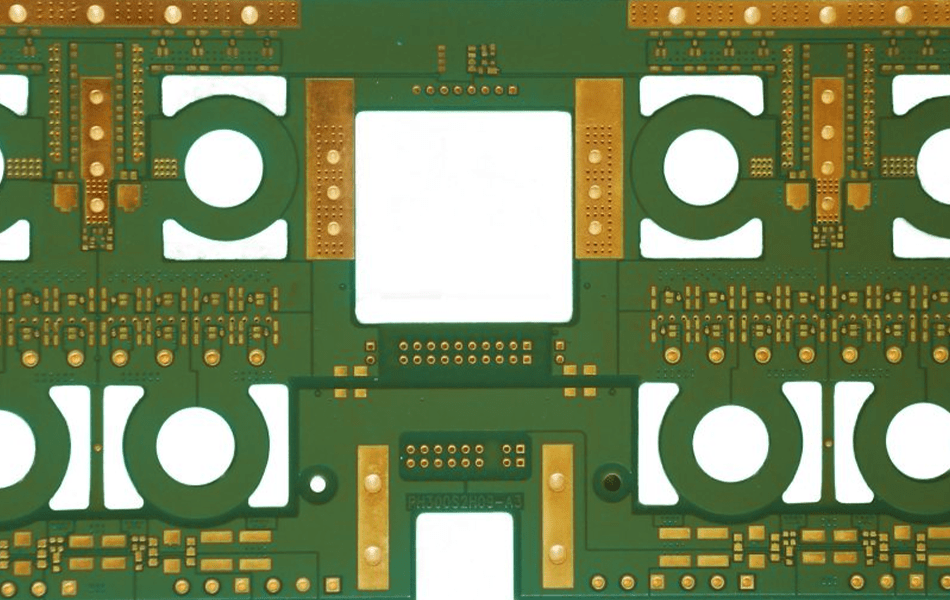
A drilled hole carries three separate promises: it has to land inside its pad, it has to present a wall that copper can bond to, and it has to be short enough that the unused length does not resonate. On FR-4 all three are routine. On PTFE they are not, because the material removes heat twenty times more slowly than copper and softens before it cuts — so the drill can smear the wall instead of severing it, and no amount of plating will repair that. These are the steps and the numbers, with the parts of the standard description that do not survive contact with a fluoropolymer.
Three Specifications in One Hole
Drilling is usually described as making connections between layers. Electrically that is right, and it hides the three tolerances a drill program actually has to satisfy.
- Position. The hole must land inside the pad with a usable annular ring left over. This is a budget shared with the lamination shrink described in the lamination guide.
- Wall. The wall has to be clean, correctly sized and free of smear, because the plating that follows bonds to what the drill left behind. A smeared PTFE wall plates, passes continuity, and fails in thermal cycling.
- Length. The unused portion of a through via is a stub, and a stub is a resonator. At 1.6 mm it rings near 23 GHz, which is why back-drilling exists.
This is step six in the twelve-step sequence, after the press and before plating. It is also the step where the material stops behaving like a generic laminate: PTFE has a thermal conductivity around 0.20 W/m·K against 0.30 for FR-4 and 385 for copper, so friction heat stays at the drill edge.
The Numbers That Define a Hole
| Parameter | Typical value | Why it matters |
|---|---|---|
| Finished hole | Drill diameter − 2 × plating | 25 µm per side means a 0.30 mm finished hole is drilled at 0.25 mm |
| Aspect ratio | ≤6:1 on PTFE, up to 10:1 on FR-4 | Sets whether plating solution reaches the hole centre |
| Hole position | ±0.05 mm | Against a 0.05 mm annular ring, one direction consumes the budget |
| Burr | ≤0.025 mm | Burrs lift the pad and shadow the plating |
| Wall roughness | Deep grooves cannot be covered by a 0.3 µm seed | |
| Hit count per tool | A few thousand, material dependent | Worn carbide burnishes PTFE instead of cutting it |
The first row is the one that gets lost between design and fabrication. A drill file released with finished diameters produces holes 0.05 mm undersize on a 25 µm-per-side plating process, which closes the annular ring and can make a 0.30 mm via too small for the component lead. The convention has to be stated, exactly as the width convention has to be stated for etching.
Step 1 — Stack Height, Entry and Backing
Drilling is done through a stack of panels, and the stack is a registration decision before it is a productivity decision. Each additional panel in the stack adds position error, so a three-panel stack on a 0.30 mm tool is normal for FR-4 and a single or two-panel stack is normal for thin PTFE.
Entry and backing material do two jobs: they stop burrs on the copper at entry, and they stop the drill from pushing laminate away at exit.
- Entry: aluminium foil 0.1–0.15 mm. It also dissipates heat from the drill tip, which matters more on PTFE than on FR-4.
- Backing: 1.5–2.5 mm phenolic or composite. On soft fluoropolymer the exit burr is the dominant defect, and a rigid backing is the cheapest way to control it.
- Pinning and datum. Panels are pinned to the same datum used in lamination and imaging. If the drill references a different datum, the registration budget is spent before the first hole.
Step 2 — Tool Geometry, and Why PTFE Needs a Sharp Edge
Carbide is universal; the geometry is where materials diverge. Two angles carry most of the difference.
Point angle. 130–140° is the working range for PCB work. A blunter point concentrates thrust, a sharper one wanders more on entry — on a 0.25 mm tool, wander is a measurable fraction of the annular ring.
Helix angle. 35–45°. The helix controls how fast the chip leaves the hole; on PTFE the chip is a soft ribbon that will re-weld to the wall if it stays in contact, so a free-cutting geometry matters more than a durable one.
Tool life is where PTFE punishes the process economically. RT/duroid 5880 is a micro-glass-fibre composite, and glass is abrasive. A tool that has drilled a few thousand hits in FR-4 still cuts FR-4; the same tool in PTFE has a rounded edge that burnishes the wall and produces smear. The rule that works is to change tools by hit count and by material, not by breakage.
Step 3 — Parameters: Two Numbers, Not One
Spindle speed and feed rate are usually quoted as a pair, which hides the two quantities that actually matter. Surface speed is what the cutting edge sees, and it is a function of diameter:
v = π × D × n → a 0.30 mm drill at 120,000 rpm runs at about 113 m/min; the same spindle speed on a 0.60 mm drill doubles it.
That is why a single spindle-speed recipe cannot be carried across a drill file: the same rpm is a different cutting condition at every diameter. The second number is chipload, the advance per revolution, typically 2–5 µm on small tools. Multiply the two and the feed rate falls out: 120,000 rpm at 3 µm per revolution is 0.36 m/min.
| Drill | Spindle speed | Surface speed | Chipload | Feed |
|---|---|---|---|---|
| 0.20 mm | 140,000 rpm | 88 m/min | 2 µm | 0.28 m/min |
| 0.30 mm | 120,000 rpm | 113 m/min | 3 µm | 0.36 m/min |
| 0.50 mm | 80,000 rpm | 126 m/min | 5 µm | 0.40 m/min |
| 1.00 mm | 40,000 rpm | 126 m/min | 10 µm | 0.40 m/min |
The values are starting points, and the rule behind them is the useful part: hold surface speed roughly constant as diameter changes, and keep chipload high enough to cut rather than rub. A low feed on a high spindle speed is the classic PTFE failure — the edge rubs, the wall heats, and the material smears.
Step 4 — The Heat Problem: Why PTFE Smears
Copper conducts heat at 385 W/m·K. FR-4 manages 0.30, RO4350B 0.69, RO3003 0.50, and unfilled PTFE such as RT/duroid 5880 about 0.20 — the worst of the family. A drill generating friction heat at the cutting edge has nowhere to send it, so the edge temperature climbs until the polymer softens.
PTFE has no true glass transition in the usual sense and melts around 327 °C. A dull edge on a low feed will reach that locally, and the result is not a cut surface but a smeared one: the polymer flows across the glass fibres, seals the wall, and hides the fibre ends that the plating chemistry needs to grip.
Smear is invisible after drilling. It is visible after plating only as a blister or a pull-away in cross-section, and in the field as a barrel that opens after thermal cycling. Three process answers, in order of effect:
- Cut, do not rub. Adequate chipload with a sharp tool. This is the fix; everything else is mitigation.
- Replace tools by hit count. A worn edge produces smear before it produces a broken hole.
- Move the heat away. Air blast and vacuum extraction at the tool, aluminium entry foil as a heat spreader, and a pause between hits on small tools rather than a continuous high-speed run.
What does not belong here is liquid coolant. Production PCB drilling is dry: the panel is a laminated dielectric with a bond interface that absorbs water, and the same moisture that causes pink ring at lamination will cause delamination and outgassing at reflow. Cooling is air and vacuum, not flood.
Step 5 — Desmear: The Chemistry That Does Not Transfer
After drilling, the wall has to be prepared for plating, and this is the second place where a generic FR-4 process fails on PTFE. FR-4 desmear works by oxidising epoxy smear with alkaline permanganate: the resin is attacked, the smear is dissolved, and the glass is left with a microscopically rough surface for the seed layer.
PTFE has no epoxy in it. Permanganate has nothing to oxidise, so a standard desmear line returns a wall that is chemically unchanged — and a fluoropolymer surface has a surface energy so low that plated copper will not bond to it at all. The two routes that work are sodium naphthalene etching, which defluorinates the surface and leaves a carbonaceous, bondable layer, and plasma treatment, which does the same job in a vacuum chamber with oxygen or hydrogen process gas.
| Material | Desmear route | What it does | Risk if skipped |
|---|---|---|---|
| FR-4 | Alkaline permanganate | Oxidises and dissolves resin smear | Wedge voids, poor adhesion |
| RO4000 (4350B / 4003C) | Permanganate, gentler | Thermoset smear, thinner than FR-4 | Resin residue on the wall |
| Ceramic PTFE (3003 / 3010) | Sodium naphthalene or plasma | Activates the fluoropolymer surface | No adhesion — barrel pulls out |
| Unfilled PTFE (5880 / TLY-5) | Sodium naphthalene or plasma | Removes smear and activates | Smear stays under the plating |
The residue from sodium naphthalene is as much of a problem as the smear it removes: it is dark, it must be rinsed thoroughly, and sodium carried into the plating bath contaminates it. The working discipline is a dedicated line, a rinse that is verified rather than timed, and a water-break check on the wall — the same 30-second test described in the inner-layer guide.
Step 6 — Registration, Annular Ring and the Budget Nobody Owns
A via lands inside its pad only if four errors fit inside the ring: drill position, panel shrink, layer-to-layer registration, and pad definition. The numbers are individually small and collectively larger than the ring.
| Contribution | Typical value | Where it comes from |
|---|---|---|
| Drill position | ±0.025–0.05 mm | Machine accuracy plus stack height |
| Panel shrink | 0.12–0.30 mm over 600 mm | Prepreg cure — compensated by scale factor |
| Layer registration | ±0.05–0.075 mm | Imaging and lamination |
| Remaining annular ring | ≥0.05 mm | What is left after the three above |
Once shrink is compensated per lot, the budget is mostly drill position and registration, and the two are correlated: a stack of three panels drilled on a machine with ±0.025 mm accuracy is not a ±0.025 mm process, because the panels move relative to each other. That is why thin PTFE builds are drilled one or two up even when the machine could take three.
Step 7 — What the Drill Decides About the RF Path
Two RF consequences are settled here and cannot be fixed later.
The stub. An unused through-via barrel is a transmission line shorted at one end. Its first resonance sits at a quarter wavelength in the filler medium: about 23 GHz at 1.6 mm, 18–19 GHz at 2.0 mm, 12 GHz at 3.2 mm. Below that frequency the stub adds capacitance and a notch appears above it. Back-drilling removes the stub with a slightly larger tool after plating, and its depth tolerance is what decides whether the remaining stub is short enough — a controlled-depth operation whose error budget is measured in tenths of a millimetre.
The wall. A rough wall is a longer conductor path and a poorer bond. At millimetre wave the current in a plated barrel is confined to a skin depth of about 0.65 µm at 10 GHz and 0.23 µm at 77 GHz, so the surface the drill leaves is literally the surface the signal uses.
Laser, Mechanical, or Both
Mechanical drilling covers through holes from about 0.2 mm upward. Below that, and for blind vias in HDI builds, laser drilling is used: UV or CO2 depending on the dielectric, with the depth controlled by energy and pulse count rather than by a physical stop.
The split matters for high-frequency work because the two processes leave different walls. A laser-drilled via in PTFE has a tapered wall and a heat-affected rim; it plates well but the taper changes the via inductance slightly and the rim has to be desmeared like any other. A mechanically drilled via in the same material has a straighter wall and a smear risk that the laser does not have. Neither is universally better — they fail differently, and the stack-up should say which one each via class expects.
Where Drilling Goes Wrong
| Symptom | Root cause in this step | Fix |
|---|---|---|
| Barrels open after thermal cycling | Smear under the plating on PTFE | Sharp tool, higher chipload, Na-naph or plasma desmear |
| Vias off-centre on one edge of the panel | Cure shrink not compensated, or a three-up stack | Per-lot scale factor; drill one or two up |
| Holes undersize after plating | Drill file released with finished diameters | State the convention; drill = finished − 2 × plating |
| Intermittent opens, coupon passes | Wall roughness deeper than the seed layer can cover | Control chipload and hit count; inspect cross-section |
| Nodules and burrs lifting pads | No entry foil or a soft backing | Aluminium entry, rigid backing, deburr |
| Narrow band of loss at 20–25 GHz | Stub resonance from an unbackdrilled through via | Back-drill to depth, or route the signal on an inner layer |
Drilling Checklist
| # | Check | Pass condition |
|---|---|---|
| 1 | Drill versus finished diameter declared | Drill = finished − 2 × plating thickness |
| 2 | Aspect ratio inside the material limit | ≤6:1 on PTFE; ≤10:1 on FR-4 |
| 3 | Stack height matches the tolerance | One or two up for thin PTFE |
| 4 | Entry foil and rigid backing | Aluminium 0.1–0.15 mm; backing 1.5–2.5 mm |
| 5 | Tool geometry suited to the resin | 130–140° point, 35–45° helix, sharp |
| 6 | Surface speed and chipload both set | v held roughly constant across diameters; 2–5 µm/rev |
| 7 | Tool change by hit count | Recorded per material, not by breakage |
| 8 | Desmear route matches the resin | Permanganate for FR-4; Na-naph or plasma for PTFE |
| 9 | Position and ring verified | ±0.05 mm position with ≥0.05 mm ring |
| 10 | Stub strategy stated | Back-drill depth or inner-layer routing for RF vias |
Conclusion
Drilling looks like the most mechanical step in the sequence and turns out to be the one where material science has the last word. The three specifications a hole carries — position, wall and length — are decided by three different things: the datum and the stack, the heat at the cutting edge, and the layer the signal is routed on.
The claims worth discarding are the ones that assume a generic laminate: that PCB drilling uses liquid coolant (it is dry, and liquid is a defect source on a laminated dielectric), that soft PTFE wants slow spindle speeds (it wants a sharp edge and a real chipload, or it smears), and that a standard permanganate desmear prepares a fluoropolymer wall (it has nothing to oxidise).
XCE PCB drills Rogers, Taconic and F4B builds with diameter-specific parameters, hit-count tool changes, sodium naphthalene or plasma desmear for PTFE, and back-drilling for RF through vias: 2–72 layers, impedance ±10%, panels to 600 × 1200 mm, 5,000 m² of production space and 80+ engineers, with samples in as fast as 24 hours. The wall these tools leave is metallised in the plating step.
Frequently Asked Questions
Do PCB drills use coolant?
Should PTFE be drilled at lower spindle speed?
How is the drill diameter chosen?
Why is aspect ratio limited on high-frequency laminates?
Can permanganate desmear be used on PTFE?
What causes a loss spike around 20–25 GHz?
Need PTFE Holes Without Smear?
Send us your Gerber files and requirements for a manufacturability review and a tailored quotation.
sales1@xcepcb.com
+86 180 3341 4657