
A hybrid stack is only as buildable as the data package that describes it. The board house cannot see your intent — it sees a Gerber set, a drill file and a drawing, and it builds exactly what those three say. Every hybrid board that came back at 61 Ω instead of 50 Ω or with the wrong laminate in it was lost in this handover, not in the routing. These are the seven deliverables, in the order they need to be fixed.
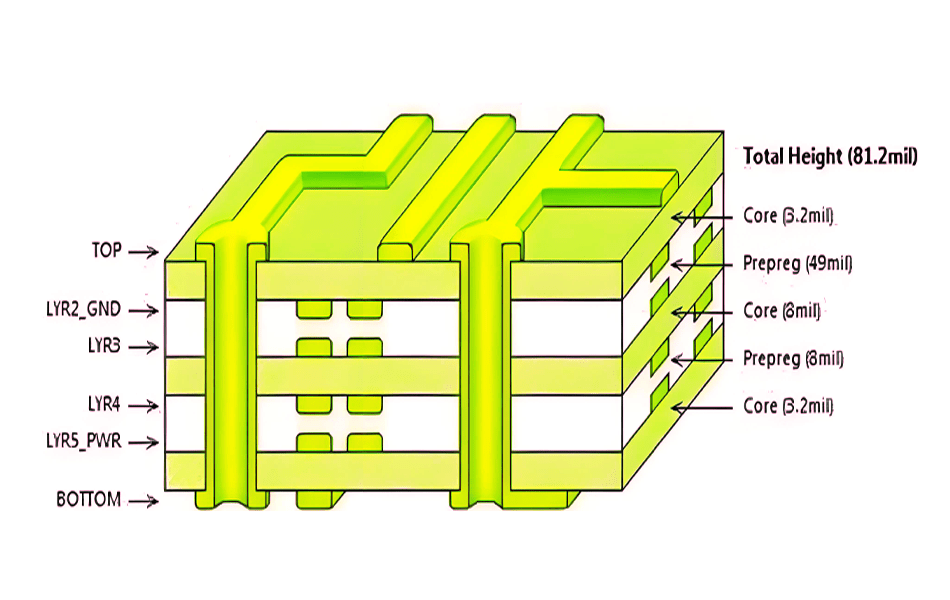
What “Mixed-Pressure” Means, and What the Package Has to Carry
The term is a literal translation of the Chinese hun ya — mixed pressing, a stack that laminates two different resin systems in one press cycle. In English fabrication language it is a hybrid or mixed-dielectric build: RO4350B or PTFE on the layers that carry RF, FR-4 on the layers that carry control, power and low-speed digital.
The electrical reason is cost. FR-4 with a Dk of about 4.3 and a loss tangent of 0.02 is fine for a gate driver and hopeless for a 24 GHz feed; a full PTFE stack would be four to six times the laminate cost for layers that never carry RF. So the stack is split, and the split is exactly where the data package gets hard.
A single-material board can be described in one sentence: material, thickness, copper. A hybrid board needs every layer identified by part number, the resin system at each interface named, the pressed height of each dielectric gap stated, and the Dk basis for every impedance calculation written down. That is the content of the next seven sections. The structural decisions behind the stack itself — how many layers, where the RF sits — are in the stack-up design guide; this article starts after those are settled.
Deliverable 1 — The Stack-Up Table, Five Columns That Cannot Be Blank
This is not the picture. It is the table the picture is drawn from, and it has to be specific enough that a substitute cannot be made without someone noticing.
| # | Layer function | Material (part number) | Dielectric | Copper | Dk basis |
|---|---|---|---|---|---|
| L1 | RF microstrip | RO4350B | 0.254 mm core | 1 oz | 3.66 design, 10–40 GHz |
| L1–L2 | Bond line | RO4450F prepreg | 0.10 mm pressed | — | Dk ≈3.5, in series |
| L2 | Solid ground | FR-4, high Tg | 0.36 mm core | 1 oz | — |
| L3 | Control / digital | FR-4, high Tg | 0.36 mm core | 0.5 oz | — |
| L4 | Power & ground pair | FR-4, high Tg | 0.36 mm core | 1 oz | — |
| L5–L6 | Mirror of L1–L2 | RO4350B + bondply | 0.254 + 0.10 mm | 1 oz | same as L1 |
Two columns carry most of the weight. Part number, because “Rogers” is a brand with more than a hundred laminates behind it: RO4003C and RO4350B differ by 0.1 in Dk, and — far more seriously — RO4003C carries no UL 94 rating while RO4350B is V-0. A vague material call on a telecom or automotive board is a compliance failure waiting for a substitute. Dk basis, because the same geometry lands at 50.0 Ω on the 3.66 design value and 51.1 Ω on the 3.48 process value, and 51.9 Ω on the 3.36 value that applies to 0.101 mm RO4350B. Without the basis printed next to the number, the next engineer re-derives the widths and the two of you disagree by 2 to 4 Ω without either being wrong.
Note also what the FR-4 rows are doing there. In a hybrid, the FR-4 layers are not filler; they are the reference planes for the RF layers. L2 is the ground that L1 sees, which is why the bondply between them belongs to the RF dielectric, not to the mechanical build.
Deliverable 2 — The Pressed Height, Not the Core Thickness
This is the single most expensive omission in hybrid packages, and it is arithmetic, not opinion. Take a 50 Ω microstrip sized the normal way: 0.56 mm wide on 0.254 mm of RO4350B. Now put the reference plane on the FR-4 side, so the gap includes a 0.10 mm bondply at Dk ≈ 3.5 in series with the core:
| Dielectric gap under the RF trace | Same 0.56 mm trace reads | Error |
|---|---|---|
| 0.254 mm (core only — what the model said) | 50.0 Ω | — |
| 0.304 mm (core + 0.05 mm bond line) | 55.8 Ω | +12% |
| 0.354 mm (core + 0.10 mm bondply) | 61.1 Ω | +22% |
| 0.404 mm (core + 0.15 mm two-ply bond) | 65.4 Ω | +31% |
Nothing exotic has happened here. Nobody substituted a material or drilled a hole in the wrong place. The board was built exactly as drawn, and it is 11 Ω out of specification because the drawing said “0.254 mm” where the electrical gap is 0.354 mm. At 50 Ω ± 10% the window is 45 to 55 Ω, so a single omitted bond line is twice the allowed tolerance.
Three rules follow. Print the pressed height of every gap, agreed with the fabricator, not the catalogue core. Include the bondply Dk in the model, because 0.1 mm of a 3.5 material in series with 0.254 mm of a 3.66 material gives an effective 3.63 for the gap — small, but it does not cancel the thickness effect. And state which side of the laminate the reference plane is on, because that is what decides whether the bond line is inside the RF field or outside it.
On PTFE hybrids the same omission gets a second life. PTFE does not flow, so the bond line is a FEP film or a low-flow prepreg that holds its thickness instead of thinning under pressure — which means the pressed height is predictable, but only if it was counted. The interface chemistry that goes with it is in the 5880 and FR-4 lamination guide.
Deliverable 3 — A DRC Run Per Material, Not Per Board
Design rule checking on a hybrid is not one pass. The RF laminate and the FR-4 obey different minimums, and a single rule set will either be too loose for the RF layers or illegally tight for the FR-4 ones.
| Rule | RO4000-class (thermoset) | PTFE (5880 / TLY-5) | FR-4 |
|---|---|---|---|
| Minimum trace / space | 0.10 / 0.10 mm | 0.15 / 0.15 mm — soft substrate, etch undercut | 0.10 / 0.10 mm |
| Via aspect ratio | ≤8:1 | ≤6:1 with Z-CTE above 200 | ≤10:1 |
| Solder mask | Standard, both sides | Adhesion limited — specify side and type, or maskless | Standard |
| Z-CTE | 32 (4350B) | 217–237 | 50–70 below Tg, 200–300 above |
| Panelisation | Standard | Score-and-break risky on thin PTFE — route, or use tabs | Standard |
The Z-CTE row is the one that needs a sentence in the fab notes rather than a rule in the tool. Where the stack changes material, the plated barrel passes through a step in expansion — 32 ppm/°C on the RO4350B side meets 50–70 below Tg and 200-plus above it on the FR-4 side, and on a PTFE hybrid the step is three to four times larger again. That is why hybrid packages carry an explicit requirement for ductile plating and a via aspect ratio limit, and why the build has to be symmetric: an unbalanced hybrid bows on cool-down and leaves permanent stress in every barrel that crosses the interface. The process side of that problem is covered in the hybrid lamination analysis.
Then the impedance half of the DRC, which is per layer and per line type. A width carried over from an RF layer to a control layer is wrong by about 7%: 0.56 mm sized on Dk 3.66 reads 46.5 Ω on FR-4 at the same height, and the correct width there is 0.498 mm — 11% narrower. On an inner stripline layer the same error is 46.1 Ω from 0.462 mm. Both are outside a ±10% window before any manufacturing tolerance is added.
Deliverable 4 — The Gerber Set, One File per Layer and Mapped to the Stack
Gerber carries geometry. It does not carry intent: no layer in a conventional Gerber set says “this pair of layers forms a 50 Ω stripline”, and no attribute says which core is RO4350B. That knowledge lives in the drawing, and the Gerber set has to be organised so the two can be matched without a phone call.
- One file per physical layer, named by layer number and function — L1_RF_top, L2_GND, L3_CTRL. Not “top / inner1 / inner2”, which breaks the moment the stack is revised.
- Gerber X2 attributes on —
.FileFunction(copper, mask, silk, profile) and.FilePolarityremove the guesswork about whether a mask layer is positive or negative. It costs one checkbox in the CAM export. - Both mask and silk on PTFE layers specified, or omitted deliberately — a mask layer that arrives by default on a PTFE board becomes an adhesion argument after the fact.
- Copper thickness per layer, in the notes if not in the attributes — 0.5 oz on an inner control layer and 1 oz on an RF layer is a normal hybrid choice and changes both etch behaviour and loss.
- ODB++ or IPC-2581 alongside the Gerber if the CAD tool can export it. These formats carry the netlist and the layer stack, which is the difference between a fabricator checking your design and a fabricator tracing your Gerbers.
What the Gerber set must not be asked to do is define the impedance. That job belongs to deliverable 6.
Deliverable 5 — Drill and Mechanical Data, Split by Span
Drill data is where hybrid boards are mis-built most often, for two reasons that are both clerical.
Finished hole versus drill size. The drawing usually quotes the finished hole, because that is what the connector pin needs. Copper plating adds 20 to 25 µm per side, so a 0.30 mm finished via is a 0.25 mm drill — and if both numbers are not stated, one of them will be wrong. State the finished size as the requirement and the drill size as derived, with the plating thickness it assumes.
One file per via span. A merged Excellon file forces the fabricator to infer which holes are through, which are blind and which are buried — and on a hybrid the inference is worse than usual, because the spans are defined by the lamination sequence, not by the layer numbers. Six-layer hybrid with an L1–L2 blind via and an L2–L5 buried via is three separate drill programmes, in three files, in the order the press cycles happen. Merged into one, the board either gets through-holes where blind vias were intended or gets drilled after the wrong press.
The mechanical drawing then carries what Gerber outlines cannot: board outline with tolerances, mounting holes and their finish, panelisation and break-away method, and the maximum panel the board will be built on. XCE PCB builds hybrid stacks to 600 × 1200 mm panels, so a large array or a long antenna board does not need to be split — but that only helps if the mechanical data says the finished size rather than leaving it to be measured off the profile.
Deliverable 6 — The Impedance Coupon Specification
At 50 Ω ± 10% the acceptance window is 45 to 55 Ω, and the coupon is the only thing that proves the board is inside it. A coupon specified as “50 Ω microstrip” proves nothing, because the fabricator will use their own coupon on their own stack. Four parameters have to be written down:
| Parameter | What to specify | Why it matters |
|---|---|---|
| Line type | Microstrip, stripline or coplanar, per layer | A 50 Ω microstrip coupon does not validate a stripline layer |
| Reference distance | The same dielectric gap as the product line | Impedance scales with h; a thicker coupon reads high and passes falsely |
| Width and length | Product width, length ≥100 mm | Width sets the value; length gives the TDR time window to separate the launch |
| Measurement | TDR, 50 Ω reference, band stated | A different method is a different number |
Two production notes. The coupon belongs on the production panel, not on a separate test vehicle, so it is pressed and drilled with the same cycle as the board. And any change to the stack — a substituted prepreg, a core that arrived 0.02 mm thin — invalidates the previous coupon, because the coupon certifies a build, not a design.
Deliverable 7 — Assembly Data, BOM and Fab Notes
The last item is the one that keeps the other six honest, because it is what a human reads before the CAM station does anything.
- Fab notes, one page — stack table reference, impedance table with coupon geometry, surface finish (ENIG against immersion silver matters at millimetre wave: 3–6 µm of nickel puts the current in a conductor with roughly a quarter of copper’s conductivity), mask type and sides, UL marking, material certificates required per lot.
- BOM split by material — the RF laminate and the FR-4 are separate line items with separate part numbers and separate thicknesses, not one line that says “PCB”.
- Pick-and-place in the fabricator’s or the assembler’s native format, with the side and rotation convention stated; the hybrid stack often puts RF components on both sides, which is where mirror errors come from.
- Revision block and file naming — one archive, one revision letter, matching the drawing. A hybrid package that exists in two versions is worse than one with no revision at all.
This is also the point where the laminate decision belongs on paper: RO4350B against RO4003C changes Dk by 0.1 and the UL rating from none to V-0, which is a supply and compliance decision before it is an electrical one. The comparison is in the 4350B versus 4003C comparison.
Where Hybrid Packages Actually Fail
Six failures account for most of the hybrid boards that come back wrong. All six are visible in the data package before anything is cut.
| What arrives | What gets built | The fix in the package |
|---|---|---|
| Material called “Rogers” | Whatever is in stock — a different Dk, and possibly a different UL rating | Part number per layer, and a no-substitution clause |
| Core thickness only | A bond line added on top — 50 Ω becomes 61 Ω | Pressed gap height, agreed with the fabricator |
| One merged drill file | Blind and buried spans inferred, drilled in the wrong cycle | One file per span, plus a lamination sequence note |
| RF width reused on FR-4 layers | 46.5 Ω — out of window before tolerances | Per-layer impedance table, not one global target |
| Coupon “50 Ω” unspecified | Fabricator’s own coupon passes on a different stack | Line type, gap, width, length, method |
| Asymmetric hybrid stack | Bow on cool-down, cracked barrels after thermal cycling | Mirror build requirement in the notes |
Every one of these is a sentence in a document. None of them can be fixed by process control after the fact, which is why the data package is worth more attention on a hybrid than on any single-material board.
Release Checklist
| # | Check | Pass condition |
|---|---|---|
| 1 | Every layer has a part number | No layer reads “Rogers”, “FR-4” or “high-frequency laminate” |
| 2 | Dk basis is written | Design or process value, with the frequency band |
| 3 | Pressed gap heights stated | Bondply and copper included; confirmed by the fabricator |
| 4 | Impedance table per layer | Target and tolerance per line type, not one global figure |
| 5 | DRC run per material class | PTFE minimums separate from FR-4 minimums |
| 6 | Gerbers named and attributed | Layer number+function in filename, X2 attributes on |
| 7 | Drill split by span | One file per span, finished and drill size both stated |
| 8 | Coupon defined | Line type, gap, width, length, method, acceptance window |
| 9 | Build is symmetric | Material class and copper weight mirrored about the centre |
| 10 | One revision, one archive | Drawing, Gerber, drill and BOM share a revision letter |
Conclusion
The routing on a hybrid board is the visible part of the design; the data package is the part that decides whether the board you get is the board you simulated. The three numbers worth remembering are 61 Ω for a forgotten bondply, 46.5 Ω for an RF width reused on an FR-4 layer, and 51.1 Ω for a design Dk quoted where the fabricator builds to the process value. All three are inside a normal working day’s carelessness, and all three are outside a ±10% window.
XCE PCB builds hybrid stacks on Rogers, Taconic and F4B laminate with impedance coupons on every RF lot: 2–72 layers, impedance ±10%, panels to 600 × 1200 mm, 5,000 m² of production space and 80+ engineers, with samples in as fast as 24 hours so a stack can be measured before tooling is committed. If the package is still being assembled, start with the design steps and the stack-up guide; for what happens once it reaches the floor, see the twelve-step manufacturing process and the impedance control steps.
Frequently Asked Questions
What are the steps for outputting hybrid high-frequency PCB design files?
Why is the pressed height different from the core thickness?
Which dielectric constant should the design use, design or process value?
Can the same trace width be reused on the FR-4 layers?
Should blind and buried vias be in one drill file?
What has to be specified on an impedance coupon?
Send Us Your Data Package for a Buildability Check
Send us your Gerber files and requirements for a manufacturability review and a tailored quotation.
sales1@xcepcb.com
+86 180 3341 4657