
Most of what determines the performance of a high-frequency board is settled before a single panel reaches the drill. The material grade, the foil roughness, the dielectric thickness, the coupon geometry and the finish are all decisions taken at the engineering review, and each of them converts into a number that the process either holds or does not. The original version of this article listed the usual headings — material, layout, impedance, etching, testing — without a single window or figure, which is why it could not be used to settle anything. This version turns those headings into twelve decisions, each with the number that has to be written down, and the tolerance that follows from it.
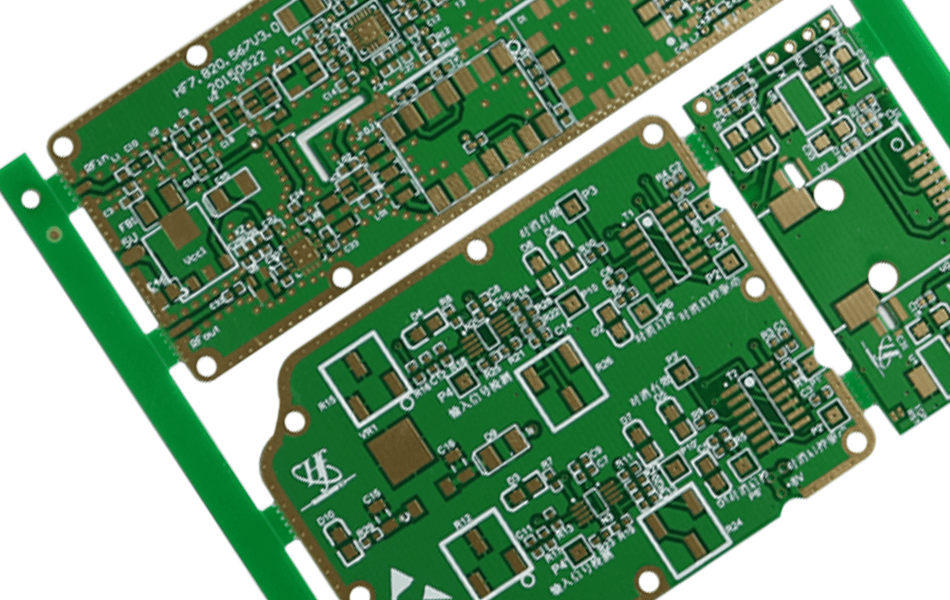
A high-frequency board fails in one of two ways. Either it never meets its loss or impedance target, because a choice made at the quotation stage was wrong, or it meets the target in the prototype and loses it in volume, because the tolerance that produced the prototype was never quantified. Both are engineering-review failures rather than shop-floor failures. Once the stack is released and the drill programme is cut, the fabricator has only the freedom the drawing gave him.
The twelve decisions below are the ones that actually consume that freedom. They are ordered the way a review runs: material, copper, stack, impedance budget, lamination, hole, fill, finish, mask, panel, coupon, acceptance. Each one is expressed as a number because a consideration without a number cannot be inspected, and a specification that cannot be inspected becomes a preference.
One comparison frames the whole article. On a 0.254 mm stack at 10 GHz, an FR-4 build loses about 1.28 dB/in of which roughly 90 % is dielectric, while an RO4003C build of the same geometry loses about 0.32 dB/in of which roughly 40 % is dielectric and the rest is copper. That single shift explains why the considerations for a high-frequency job are not the FR-4 list with better material substituted: the binding constraint moves from the laminate to the copper surface and the finish.
Dielectric loss per unit length follows the attenuation relation αd ≈ 2.6 · fGHz · √Dk · Df in dB/in. Two consequences matter for selection. Loss rises linearly with frequency, so a grade that is adequate at 3 GHz is not automatically adequate at 10 GHz. And loss scales with the square root of Dk, which means a high-Dk material pays a penalty on every millimetre of dielectric — not because high Dk is inherently lossy, but because the same electrical length is shorter in physical terms and the loss per unit of electrical length is unchanged. High Dk saves area; it does not save decibels.
| Grade | Dk (process) | Df | Dielectric loss at 10 GHz | Where it stops being the right answer |
|---|---|---|---|---|
| Generic FR-4 | 4.3–4.6 | 0.016–0.025 | about 1.08 dB/in | Above roughly 2–3 GHz on any run longer than a few centimetres |
| RO4350B | 3.48 ±0.05 | 0.0037 | 0.18 dB/in | Above about 10 GHz on loss-critical links; still the cheapest route to controlled impedance |
| RO4003C | 3.38 ±0.05 | 0.0027 | 0.13 dB/in | Millimetre wave, where 0.13 becomes a measurable fraction of the budget |
| RO3003 | 3.00 ±0.04 | 0.0010 | 0.045 dB/in | Cost; and thin cores are mechanically soft |
| RT/duroid 5880 | 2.20 ±0.02 | 0.0009 | 0.035 dB/in | Dimensional stability and plated-hole reliability at fine geometry |
| Taconic TLY-5 | 2.20 ±0.02 | 0.0009 | 0.035 dB/in | Same class as 5880; a second source rather than a different design point |
The grade alone does not fix the loss, because dielectric constant is a function of temperature. RT/duroid 5880 drifts about −125 ppm/°C, RO4003C about +40 ppm/°C and RO4350B about +50 ppm/°C. A 100 °C excursion therefore moves a 5880 design by roughly 1.2 % in Dk and a 4350B design by about 0.5 % in the opposite direction, which translates into an impedance shift of 0.3–0.7 Ω and, more importantly, into a phase shift that matters in a phased array. The sign of the coefficient is a design parameter, not a datasheet footnote; it is what separates a stable array from one that needs recalibration over temperature.
The practical rule at review is to write the loss budget in dB, divide it between dielectric and copper, and then check that the chosen grade leaves headroom for the finish. A 10 GHz link with a 3 dB budget over 150 mm of line has 0.5 dB/in available; a 4003C stack consumes 0.13 of that in dielectric and roughly 0.19 in copper at standard foil, which is why the foil decision in the next section is not optional.
At 10 GHz the current in copper occupies about 0.65 µm of depth. Standard electrodeposited foil has an rms surface roughness of 2–3 µm, so the current path is several times longer than the geometric length of the trace. The correction is usually written as a roughness factor applied to the smooth-copper loss:
K = 1 + (2/π) · arctan[1.4 · (Δ/δ)²], where Δ is the rms roughness and δ the skin depth
| Foil class | Rms roughness Δ | K at 10 GHz (δ = 0.65 µm) | Copper loss, 0.254 mm line, Dk 3.38 | Where it is justified |
|---|---|---|---|---|
| Standard ED | 2.5–3 µm | about 1.9 | about 0.19 dB/in | Sub-6 GHz, short runs, cost-driven |
| Reverse-treated (RTF) | 1.5–2 µm | about 1.7 | about 0.17 dB/in | General multilayer, 6–12 GHz |
| HVLP / VLP | 0.5–1 µm | about 1.45 | about 0.145 dB/in | Above 10 GHz, or any loss budget under 0.4 dB/in |
| Rolled annealed (RA) | 0.3–0.5 µm | about 1.35 | about 0.135 dB/in | Flexible and thin PTFE builds |
Two things follow that are routinely missed. First, the gain from smooth foil is largest where the dielectric loss is smallest: on FR-4 the copper term is under 10 % of the total, so paying for HVLP there buys almost nothing, while on 5880 the copper term is over 80 % of the total, so foil roughness is the dominant lever. Second, roughness is not only a loss parameter; it changes the effective Dk of the laminate at high frequency, because the resin-rich layer at the foil interface behaves electrically like a thin layer of a different material. That is why the design Dk and the process Dk differ in every high-frequency datasheet, and why the impedance model has to be built on process Dk.
The review question is therefore not “which copper weight” but “which foil, on which face, with which Dk model”. Copper weight still matters for current and for the etched trapezoid, as the guide to PCB copper foils sets out foil by foil, but at 10 GHz above the skin depth, extra copper weight adds almost nothing to conduction and instead costs etch resolution.
Characteristic impedance fixes a ratio, not a width. For a microstrip on Dk 3.38 the 50 Ω solution is a fixed W/h of about 2.33, so the trace width is a consequence of the dielectric thickness. Any discussion that starts from a desired trace width is a discussion about changing the board thickness, and it is much cheaper to have that discussion before lamination than after.
| Dielectric thickness | 50 Ω width, Dk 3.38 | 50 Ω width, Dk 2.20 (5880) | Effect of ±25 µm etch on that width |
|---|---|---|---|
| 0.102 mm | 0.24 mm | 0.32 mm | 10 % — outside any ±5 % impedance window |
| 0.203 mm | 0.47 mm | 0.63 mm | 5.3 % — needs etch compensation per panel |
| 0.254 mm | 0.59 mm | 0.79 mm | 4.2 % — the common microwave case |
| 0.508 mm | 1.18 mm | 1.58 mm | 2.1 % — convenient tolerance, thick board |
| 0.813 mm | 1.89 mm | 2.53 mm | 1.3 % — antenna feeds, high power |
Stripline changes the number by roughly a factor of 2.5: because the field is confined between two ground planes, a 50 Ω stripline in the same dielectric is about 2.5 times narrower than the microstrip. That is bought with a much tighter thickness tolerance, because the impedance now depends on two dielectric layers in series and the sum of their tolerances. A stripline stack quoted at ±10 % thickness is a ±6 % impedance stack before any etch error is added.
For thin cores there is a further constraint that has nothing to do with impedance: below about 0.1 mm the core no longer behaves as a mechanical datum, and thin PTFE in particular creeps under lamination pressure. A 0.102 mm 5880 core compressed by 4 % cold flow takes a 50 Ω design to 48.8 Ω, which is most of a ±3 % window spent on a process artefact rather than a design choice. Stack design for PTFE therefore keeps dielectric thickness at 0.254 mm or above wherever the mechanical envelope allows, which is the argument developed in high-frequency PCB stack-up design.
A quoted impedance tolerance is meaningless until the contributors are listed. The table below is the budget used at review for a 50 Ω microstrip on 0.254 mm RO4003C; the point of writing it out is that the thickness term dominates, which is not where most design effort goes.
| Contributor | Typical window | Effect on 50 Ω | Who controls it |
|---|---|---|---|
| Dielectric thickness | ±10 % (standard laminate spec) | ±6 % | Laminate supplier and press cycle |
| Etched width | ±25 µm | ±2.8 % at 0.59 mm; ±5.5 % at 0.254 mm line | Etch compensation in CAM |
| Dk tolerance | ±0.05 on 3.38 | ±0.7 % | Laminate supplier |
| Plating build-up on outer layers | +20–25 µm | −1 to −2 Ω | Pattern plating current density |
| Solder mask over the trace | 20–30 µm | −1 to −3 Ω | Design, by mask opening |
| A bondply layer left out of the model | 0.10 mm | +22 % (50 → 61.1 Ω) | Whoever wrote the stack |
| Void or air gap in the dielectric | 10 µm | +2.3 Ω | Press vacuum and flow |
Read down the right-hand column and the priorities become obvious. Thickness and width are the two that can be controlled at the fabricator; the bondply omission is the one that produces a board that is 20 % off and cannot be fixed, because it is a modelling error rather than a process error. On a hybrid stack, where an FR-4 prepreg bonds a 4350B core, that layer is part of the transmission line and has to be in the field solver, not in the mechanical drawing only. The measurement side of the same budget is covered in impedance control in high-frequency PCB manufacturing.
Three laminate families cure in three different windows, and they cannot be cured in one cycle. That single fact decides how many press operations a build needs, and therefore a large part of its cost and its yield.
| System | Bond temperature | Pressure / vacuum | Can it be co-cured with the others? |
|---|---|---|---|
| FR-4 (epoxy) | 170–190 °C | 200–350 psi, vacuum <50 mbar | Bonds to RO4000 through a hydrocarbon-compatible prepreg at 190–200 °C |
| RO4000 series (hydrocarbon / ceramic thermoset) | 190–200 °C | 200–400 psi | Bonds to FR-4 in the same cycle only with the matching prepreg, never with PTFE |
| PTFE with FEP bonding film | 260–300 °C | 200–500 psi, slow ramp | No — a separate cycle, or a low-flow prepreg at 180–190 °C |
The cost consequence is arithmetic. A four-layer hybrid of FR-4 and 4350B is one press cycle; a four-layer hybrid of FR-4 and 5880 is at least two, plus a bonding film, plus a second drill and imaging sequence if the PTFE layer is inner. That is why the “we will just use PTFE where it matters” instruction, given without a layer allocation, usually comes back as either a much higher price or a much worse yield.
Two process numbers belong in the same decision. Prepreg shrinks 0.02–0.05 % on cure, which is 0.12–0.30 mm across a 600 mm panel — larger than most layer-to-layer registration budgets, so it has to be compensated per layer rather than absorbed. And PTFE cold-flows under pressure: a 0.254 mm core that loses 4 % of its thickness moves a 50 Ω line to 48.8 Ω. Both numbers are the reason lamination is treated as a design decision rather than a shop-floor step.
PTFE behaves differently at every hole-making step, and the differences are not marginal.
| Step | FR-4 / RO4000 | PTFE (5880, TLY-5) | Why |
|---|---|---|---|
| Desmear | Permanganate, standard cycle | Sodium naphthalenide or plasma only | PTFE is not attacked by permanganate; the smear stays and the barrel opens intermittently |
| Aspect ratio ceiling | 8:1 to 10:1 | about 6:1 | Limited throw into a non-wetting surface, and Z-axis expansion of 80 µm at reflow |
| Z expansion, 1.6 mm through 215 °C | 17–24 µm (FR-4), about 11 µm (4350B) | about 82 µm (5880), about 75 µm (TLY-5) | CTE of 237 ppm/°C in Z versus 46 for 4003C |
| Plating ductility | ≥15 % elongation | ≥20 % elongation | The barrel has to stretch with the laminate, not resist it |
| Finished hole tolerance | ±50 µm typical | ±50 µm, on a hole 2 × 25 µm smaller than the drill | Copper thickness is subtracted from the drill diameter, not added |
The desmear line is the one that costs most when it is wrong, because the failure is intermittent rather than visual. A barrel that is 90 % connected passes continuity, passes thermal shock, and opens in the field after a few hundred cycles. This is why high-frequency boards are qualified by cross-section and not by electrical test alone, and why drilling and plating are reviewed against the laminate rather than against a generic recipe.
Resin plugging is treated as a finish option when it is really a thickness-dependent process. On a 1.6 mm board, filling a 0.3 mm via is a contained operation: paste is pressed in, cured, and planarised. On a 0.203 mm board the same operation has nowhere to put the displacement. The paste volume has to go somewhere, and the only compliant thing in the stack is the dielectric, which compresses; on PTFE it cold-flows, and on any laminate the bake that cures the paste shrinks the board in the plane.
Three consequences follow, and all three are measurable. The dielectric under the filled via thins, which raises the local capacitance and drops the impedance by a few ohms under the pad. The board shrinks in X-Y during cure, which moves the registration of everything already drilled. And the fill itself shows voids and dish-down at the surface, which the assembly house then tries to solve with more paste. Below about 0.25 mm, the honest options are plated-over vias with no fill, or a different construction — which is the argument made in resin plugging in high-frequency boards.
Surface finish is usually specified for solderability and shelf life. On a high-frequency board it is an electrical layer, and the comparison is decided by one number: at 10 GHz the skin depth is 0.65 µm in copper and 1.33 µm in nickel. Any nickel layer thicker than that carries the current at a resistivity roughly four times that of copper.
| Finish | Typical thickness | Effect at 10 GHz | Use it when |
|---|---|---|---|
| OSP | 0.2–0.5 µm organic | Lowest insertion loss; no metal added | The board is assembled within months; loss matters more than shelf life |
| Immersion silver | 0.1–0.3 µm | Close to OSP; slight tarnish and silver migration risk | Long storage with high-frequency performance, controlled atmosphere |
| ENIG | Ni 3–6 µm + Au 0.05–0.1 µm | Surface resistance about 2 × copper; usable to roughly 10 GHz | Fine pitch, wire bonding, long shelf life |
| ENEPIG | Ni + Pd + Au | Same nickel penalty as ENIG | Gold wire bonding and repeated reflow |
| Hard gold on connector fingers | 0.5–1.5 µm over Ni | Nickel and cobalt under the gold dominate the loss | Edge connectors only, not transmission line |
The decision is not aesthetic. A 20 mm launch through ENIG at 20 GHz can add a measurable fraction of a decibel that no amount of laminate improvement will recover, because the loss is in the finish, not in the dielectric. The full comparison of the eight common finishes is in PCB surface treatment processes; the review-level rule is simply that RF launch areas and anything above 10 GHz default to OSP or immersion silver unless the assembly process forbids it.
Solder mask is a dielectric with a Dk between roughly 3.5 and 4.5, and white legend ink is worse at around 6.5. Over a 0.254 mm microstrip the mask adds 20–30 µm of a higher-Dk material on top of the trace, which lowers the impedance by 1–3 Ω and raises the loss slightly. Over a coplanar gap it does more, because the field is concentrated in the gap and the mask fills it.
The controllable responses, in order of effectiveness: open the mask over the impedance-critical trace (a “mask dam” design that the assembly house accepts if there is no exposed copper to solder), keep the mask thickness at the low end of the window, and never place legend over a matched line. Mask openings are free in the artwork; a 2 Ω impedance error discovered after assembly is not. The number to write on the drawing is the mask-opening geometry on the impedance layers, not the mask colour.
High-frequency laminates are bought in 600×1200 mm sheets more often than in any other format, so the panel that is quoted is usually a subdivision of that sheet. Utilisation is the first-order cost driver, and it is set at the drawing stage rather than in the CAM department.
| Array choice on a 600×1200 sheet | Utilisation | Boards per sheet | Trade |
|---|---|---|---|
| 100×100 mm, 5×11 with rails | about 76 % | 55 | Good balance; enough border for tooling and coupons |
| 120×160 mm, 4×7 with rails | about 74 % | 28 | Fewer handling steps, larger per-board risk |
| 80×80 mm, 7×14 with rails | about 82 % | 98 | Best material yield; more routing and more handling |
| Single board 200×300 mm | about 50 % | 4 | Only for very large antennas; border is wasted material |
Utilisation is also a tolerance question. A panel needs 5–8 mm of border for tooling holes and for the fiducials that the LDI and the drill reference to, and it needs a copper-balanced area for the impedance coupon. Placing the coupon in the open border is the classic mistake: the border etches differently from the interior, so the coupon measures a line that does not exist on the board. The same panel-level reasoning governs whether the array is routed or V-scored, since V-scoring on PTFE risks delamination at the score line.
An impedance specification without a defined coupon is a specification without a measurement. Three things have to be on the drawing: the coupon geometry per layer and per impedance target, the test method, and the acceptance frequency. A coupon that is 50 Ω at 1 GHz is not evidence that the line is 50 Ω at 10 GHz, because the effective Dk and the copper loss both move with frequency.
Time-domain reflectometry is fast and resolves discontinuities, but its spatial resolution is set by the rise time: a 35 ps edge resolves features of about 3.5 mm, which is adequate for a coupon and not adequate for a connector launch. Vector network analysis with a proper calibration gives impedance and loss in the frequency domain, which is what a link budget needs. The practical arrangement is a coupon per layer with both a TDR trace and an S-parameter measurement, sampled at the centre and the edge of the panel, since the etch rate differs between the two.
The review point is that the coupon costs a few square centimetres and settles arguments for the life of the part number. Without it, the acceptance criterion becomes a conversation about whose measurement was more representative, and the answer is usually the one held by whoever has the invoice.
The last decision is what the board will be judged against, and by whom. For high-frequency multilayer work the useful reference set is IPC-A-600G for the workmanship visible in cross-section and on the surface, and IPC-6015 for the performance requirements of the finished board, plus the coupon data. Those three together decide whether a barrel with 20 % void is a reject or a concession.
The first-article gate is where the twelve decisions are tested at once. A first article should include a cross-section at the worst-case aspect ratio, coupon impedance against the budget, a thermal shock of at least 3 cycles at 288 °C or the reflow-equivalent, and a dimensional check on the layer-to-layer registration. If the first article passes all four, the process is in control; if it passes only the electrical tests, the process is lucky.
| Decision | The number to write down | Who owns it | How it is verified |
|---|---|---|---|
| 1. Grade | Df and Dk, with the loss budget in dB/in | Design | Datasheet plus coupon loss |
| 2. Foil | Roughness class and face | Design and purchasing | Supplier certificate, coupon loss |
| 3. Stack | Dielectric thickness per layer, ±10 % | Design | Cross-section |
| 4. Impedance budget | Contributor list, not a single ±% | Design and process engineering | Coupon statistics |
| 5. Lamination route | Number of press cycles, peak temperature | Process engineering | Press records, cross-section |
| 6. Hole | Aspect ratio, desmear chemistry | Process engineering | Cross-section after thermal shock |
| 7. Fill | Board thickness versus fill feasibility | Design | Micro-section of a filled via |
| 8. Finish | Metal system and thickness | Design | XRF plus coupon loss |
| 9. Mask | Opening geometry on impedance layers | Design | AOI, coupon before and after |
| 10. Panel | Array, utilisation, coupon position | CAM | Panel drawing, coupon location |
| 11. Coupon | Geometry, method, frequency | Design and test | TDR and VNA reports |
| 12. Acceptance | IPC-A-600G, IPC-6015, coupon limits | Quality | First article, then sampling |
The twelve decisions share a shape: each one converts a preference into a number that a process can hold or miss, and each one is cheaper to make before the artwork is released than after. The three that most often go wrong are the ones that look like bookkeeping rather than engineering — the foil face, the bondply layer in the impedance model, and the coupon definition — because none of them shows up in a schematic and all of them survive into the finished board.
The order matters as much as the content. Material and foil set the loss floor; the stack sets the width; the lamination route sets the cost and the registration; the hole and the fill set the reliability; the finish and the mask set the last few tenths of a decibel; and the coupon and the acceptance standard decide whether any of it can be demonstrated. A build that settles all twelve can be argued about on the basis of measurements. A build that settles six can only be argued about on the basis of opinion.
XCE PCB reviews high-frequency jobs against this list before releasing tooling: 2 to 72 layers, PTFE, hydrocarbon and ceramic laminates, 600×1200 mm panels, impedance held to ±10 %, samples in as fast as 24 hours, inspected to IPC-A-600G and IPC-6015. The station-by-station windows that follow from these decisions are set out in considerations in the production process of high-frequency PCBs, and the microwave-specific case in the production process of microwave PCBs.
Send us your Gerber files and requirements for a manufacturability review and a tailored quotation.